welcome to Jixiang E-commerce!

Blog

Home

Blog

  • Nitrile vs Latex vs PVC Gloves - Material Properties and Task Fit (2026 Comparison)
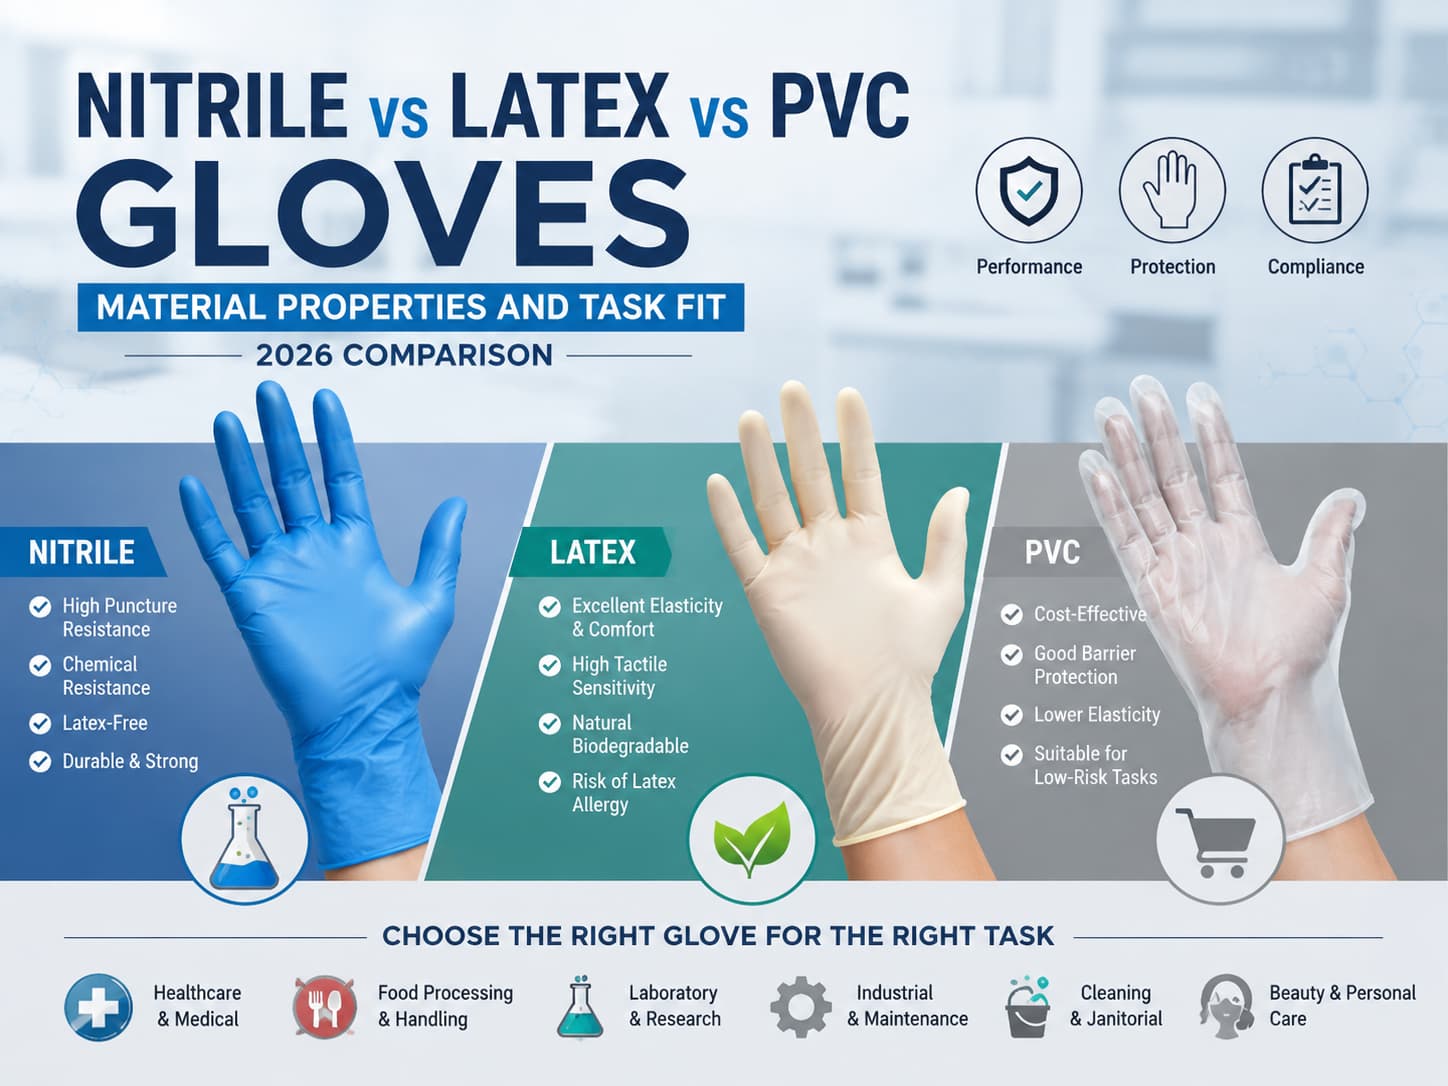
    Nitrile vs Latex vs PVC Gloves - Material Properties and Task Fit (2026 Comparison)
    Sep 03, 2026
    Nitrile, latex, and PVC gloves each have different strengths. This comparison explains the chemistry, barrier performance, allergy risks, and best-use tasks for each material so buyers can match the glove to the job. The three most common disposable glove materials - nitrile rubber, natural rubber latex, and polyvinyl chloride (PVC) - are not interchangeable. Each has a different polymer structure, barrier profile, elasticity, allergy risk, and cost base. The right choice depends on the task, the regulatory environment, and the user population. This guide compares the materials side by side and provides a task-based selection framework. 1. The Chemistry in One Sentence Nitrile rubber is acrylonitrile butadiene rubber (ACN + butadiene), a synthetic polymer with no latex proteins Natural rubber latex is a plant-derived polymer harvested from Hevea brasiliensis trees; it contains proteins that can trigger Type I allergy PVC is a thermoplastic polymer made from vinyl chloride monomer, softened with plasticizers such as phthalates or DINCH for glove use 2. Side-by-Side Material Comparison Property Nitrile rubber Natural rubber latex PVC / vinyl Source Synthetic (ACN + butadiene) Natural (Hevea tree latex) Synthetic (vinyl chloride) Latex proteins None Present None Tensile strength High (>= 14 MPa per ASTM D6319) Very high (18-24 MPa typical) Moderate (8-13 MPa typical) Elongation at break 400-600% 650-750% 250-350% Puncture resistance Excellent Good Lower Chemical resistance Best (oils, solvents, many chemicals) Moderate Limited (better with acids/bases) Tactile sensitivity Very good, especially thin grades Excellent Fair Allergy risk Type I: none; Type IV: possible (accelerator chemicals) Type I: yes; Type IV: possible Type I: none; plasticizer/Type IV: possible Cost position (2026) Mid-to-premium Moderate Lowest Common thickness 3-8 mil (0.08-0.20 mm) 3-7 mil (0.08-0.18 mm) 3-5 mil (0.08-0.13 mm) 3. Barrier Performance Against Pathogens and Chemicals For medical and food safety, the most important question is whether the glove blocks pathogens and the chemicals it will contact. Nitrile rubber generally outperforms latex and PVC for oils, solvents, and many hospital chemicals. Latex has excellent barrier properties for biological fluids but is degraded by oils. PVC is acceptable for low-risk tasks and short-duration contact but has lower puncture resistance and can soften or leak under stress. 4. Allergy Considerations Type I latex allergy is the headline risk for natural rubber latex gloves. It can cause hives, respiratory symptoms, and anaphylaxis. Nitrile and PVC gloves eliminate this risk. However, nitrile gloves can still trigger Type IV contact dermatitis in some users because of accelerator chemicals such as thiurams, carbamates, and mercaptobenzothiazole (MBT). Accelerator-free nitrile gloves are available for sensitive users. 5. Cost and Supply Factors in 2026 Raw material costs influence glove pricing. Nitrile rubber depends on acrylonitrile and butadiene, both petrochemical derivatives; prices can rise with crude oil and cracker economics. Natural rubber latex depends on plantation supply, weather, and the TSR20 price. PVC is tied to PVC resin and plasticizer costs, which are generally the lowest of the three. As of late August 2026, Brent crude has risen above $89/barrel on Middle East tensions, putting upward pressure on nitrile feedstock costs, while PVC resin remains relatively soft. 6. Task-Based Selection Guide Task / Industry Recommended material Why Medical examination Nitrile rubber Latex-free, strong barrier, puncture-resistant, meets ASTM D6319 / EN 455 Surgery Natural rubber latex or synthetic polyisoprene Best tactile sensitivity and elasticity; low-protein powder-free grades required Chemotherapy handling Thick nitrile (ASTM D6978 tested) Resists permeation by oncology drugs Food handling Nitrile or PVC Cost-effective, complies with FDA 21 CFR 177.2600 / EU 1935/2004 Industrial / automotive Nitrile Oil and solvent resistance Cleanroom / electronics Powder-free nitrile or latex Low particle shedding; chemical compatibility Short low-risk cleaning PVC Lowest cost; adequate for brief contact Tattoo / beauty Nitrile Barrier to inks and blood; latex-free for client safety 7. Procurement Checklist Assess the hazard: biological, chemical, mechanical, or combination Screen users for latex allergy: if any risk exists, default to nitrile or PVC Match thickness to task: 3-4 mil for dexterity; 6-8 mil for durability Request certifications: EN 455 or ASTM D6319 for medical; FDA 21 CFR 177.2600 or EU 1935/2004 for food Consider accelerator-free nitrile: for users with Type IV dermatitis Check raw material trends: lock in pricing when butadiene/ACN costs are rising Data sources: ASTM D6319; EN 455 series; EN ISO 21420:2020 (formerly EN 420); FDA 21 CFR 177.2600; EU 1935/2004; ASTM D6978; material property data from major glove manufacturers. Information current as of August 2026. FAQ Q: Which glove material is best for chemical resistance? A: Nitrile rubber generally offers the best chemical resistance among the three common disposable glove materials, especially against oils, greases, solvents, and many hospital chemicals. Latex performs well against biological fluids but is degraded by oils and hydrocarbons. PVC has limited chemical resistance and is best for short-duration, low-risk contact. Q: Are nitrile gloves completely allergy-free? A: Nitrile gloves eliminate Type I latex allergy because they contain no latex proteins. However, some users may develop Type IV contact dermatitis from accelerator chemicals used in the vulcanization process, such as thiurams, carbamates, and mercaptobenzothiazole (MBT). Accelerator-free nitrile gloves are available for these users. Q: Why are PVC gloves cheaper than nitrile and latex? A: PVC gloves are cheaper because PVC resin and plasticizer raw materials are generally lower-cost than nitrile rubber monomers (acrylonitrile and butadiene) or natural rubber latex. They are also simpler to manufacture. The trade-off is lower puncture resistance, lower elasticity, and more limited chemical resistance. Q: Can latex gloves be used for food handling? A: Yes, powder-free latex gloves can be used for food handling where permitted, but many food businesses avoid them because of Type I latex allergy risk among workers and customers. Nitrile and PVC are more common choices in food service because they are latex-free. Q: Which material has the best tactile sensitivity? A: Natural rubber latex has the best tactile sensitivity and elasticity, which is why it remains preferred for surgical applications. Modern thin nitrile gloves (3-4 mil) can approach latex-like sensitivity for most examination tasks, while PVC is generally less tactile.  
  • ISO 14644 Cleanroom Gloves: Particle Control and Selection Guide for Pharma and Electronics (2026)
    ISO 14644 Cleanroom Gloves: Particle Control and Selection Guide for Pharma and Electronics (2026)
    Aug 31, 2026
    ISO 14644 cleanroom gloves are disposable gloves engineered for controlled environments where airborne particles must be minimized. This guide explains cleanroom classifications, particle limits, material selection, and testing standards for pharmaceutical and electronics manufacturing. ISO 14644 cleanroom gloves are disposable gloves designed and manufactured for controlled environments where airborne particles, ionic contamination, and extractable residues must be kept within strict limits. Unlike general medical or industrial gloves, cleanroom gloves are washed, packaged, and tested specifically to reduce particle shedding and outgassing. They are used in pharmaceutical compounding, semiconductor fabrication, aerospace assembly, biotechnology, and medical device manufacturing. This guide explains the ISO 14644 classification system, how to match a glove to a cleanroom class, and what testing data buyers should request. 1. What Is ISO 14644? ISO 14644 is the international family of standards for cleanrooms and associated controlled environments. Part 1 (ISO 14644-1:2015) defines cleanroom classes by the maximum concentration of airborne particles per cubic meter. The lower the class number, the cleaner the environment. Gloves used in these rooms must themselves not become a particle source. ISO 14644-1 class Max particles >= 0.5 micrometres / m3 Max particles >= 5.0 micrometres / m3 Typical glove requirement ISO Class 3 35 0 (not defined) Specialized gloves; very low particle shedding ISO Class 4 352 3 Low-shedding nitrile or latex ISO Class 5 3,520 29 High-quality nitrile, double-bagged ISO Class 6 35,200 293 Nitrile or latex, cleaned and packaged ISO Class 7 352,000 2,930 Standard cleanroom-grade gloves ISO Class 8 3,520,000 29,300 Cleanroom-compatible gloves 2. Why Gloves Matter in a Cleanroom A human hand is a major source of particles, skin flakes, oils, and microorganisms. A glove is the barrier between the operator and the product. But if the glove itself sheds particles, releases plasticizers, or holds ionic residues, it becomes a contamination source. Cleanroom gloves are therefore subjected to additional controls beyond standard medical glove testing: Particle shedding: measured by methods such as IEST-RP-CC005 to count particles released during wear or flexing Ionic contamination: tested for chloride, sodium, potassium, and other ions that can corrode electronics Non-volatile residue (NVR): measures extractable organic and inorganic residues left after solvent extraction Silicone and amide content: critical for electronics and aerospace where residue causes defects Bioburden: especially important for aseptic pharmaceutical operations 3. Material Selection: Nitrile, Latex, and PVC Most cleanroom gloves are made from nitrile rubber or natural rubber latex. PVC is rarely used in high-grade cleanrooms because of plasticizer migration and higher particle counts. The table below compares the three materials for cleanroom use. Material Particle shedding Chemical resistance Allergy risk Common cleanroom use Nitrile rubber Low (especially chlorinated, powder-free) Good (oils, solvents) Type I latex-free; low Type IV with accelerator-free grades Semiconductor, pharma, biotech Natural rubber latex Very low in high-grade cleanroom grades Moderate Type I protein allergy risk Pharma, laboratory (declining due to allergy policy) PVC / vinyl Higher than nitrile/latex Limited Low protein risk; plasticizer concerns Low-grade controlled areas only 4. Thickness and Dexterity Cleanroom work often involves handling small components, vials, or wafers. Glove thickness is therefore a trade-off between tactile sensitivity and chemical or tear resistance. Cleanroom gloves are typically 3.5-6.0 mil (0.09-0.15 mm) in thickness. Dexterity ratings under EN ISO 21420 (formerly EN 420) range from 1 to 5, with 5 being the most dexterous; cleanroom tasks usually require dexterity level 4 or 5. 5. Standards and Test Methods to Request Buyers should ask suppliers for cleanroom-specific test reports in addition to standard medical glove certificates: ISO 14644-1: confirms the target cleanroom class the glove is suitable for IEST-RP-CC005: recommended practice for glove and finger cot testing in cleanrooms, covering particles, extractables, and ions ASTM D6319 or EN 455: baseline medical/examination glove physical properties ISO 10993-5 / ISO 10993-10: cytotoxicity and sensitization testing EN ISO 21420 (formerly EN 420): general glove requirements including pH, innocuousness, and dexterity 6. Packaging and Handling Rules Even a clean glove becomes contaminated if it is not packaged correctly. Cleanroom gloves are typically: Cleaned with deionized water to remove surface particles and ions Packaged in double bags so the outer bag can be removed before entering the cleaner zone Labeled with lot number, manufacturing date, expiry date, and cleanroom class claim Stored away from direct light, heat, and humidity to prevent material degradation 7. Buyer Checklist for Cleanroom Glove Procurement Define the cleanroom class: match the glove to the ISO 14644-1 class of your operation Request particle and ionic test data: do not rely only on medical glove certificates Choose nitrile for high-grade rooms: nitrile rubber gloves offer the best balance of low shedding, chemical resistance, and latex-free safety Verify accelerator-free options: if operators show Type IV sensitivity, specify accelerator-free nitrile Check double-bagging and labeling: ensure the packaging supports your entry protocol Audit the supplier's cleanroom washing line: not every glove factory has dedicated cleanroom finishing equipment Data sources: ISO 14644-1:2015; IEST-RP-CC005; EN ISO 21420:2020 (formerly EN 420); ASTM D6319; EN 455 series; ISO 10993 series. Information current as of August 2026; verify specific cleanroom requirements with your facility qualification. FAQ Q: What is the difference between ISO 14644-1 Class 5 and Class 7 cleanroom gloves? A: The difference is the maximum allowable particle concentration. ISO Class 5 permits no more than 3,520 particles of 0.5 micrometres or larger per cubic metre, while ISO Class 7 permits up to 352,000 such particles. Gloves for Class 5 must release far fewer particles during flexing and wear, so they are usually higher-grade nitrile or latex that has been washed and double-bagged. Class 7 gloves can be standard cleanroom-compatible gloves with less stringent particle limits. Q: Are latex gloves allowed in cleanrooms? A: Yes, but their use is declining. Natural rubber latex gloves can be manufactured to very low particle-shedding levels and are still used in some pharmaceutical and laboratory cleanrooms. However, they carry a Type I latex protein allergy risk, so many facilities have moved to latex-free nitrile gloves to protect operators and avoid protein contamination. Q: What tests prove a glove is suitable for a cleanroom? A: The most common cleanroom-specific tests are IEST-RP-CC005 (particle shedding, extractables, and ionic contamination), non-volatile residue (NVR) testing, and silicone/amide analysis for electronics. Buyers should also request baseline medical glove data such as ASTM D6319 or EN 455 physical properties, plus ISO 10993 biocompatibility reports. Q: Can I use standard medical nitrile gloves in a cleanroom? A: Not without verification. Standard medical nitrile gloves may meet ASTM D6319 or EN 455 for barrier and strength, but they are not necessarily washed or packaged to reduce particle shedding. For cleanroom use, you need gloves that have been specifically processed, tested for particles and ions, and double-bagged for cleanroom entry. Q: Why is double-bagging important for cleanroom gloves? A: Double-bagging creates a buffer between the outer shipping carton - which has been exposed to warehouse and transport environments - and the clean interior. The outer bag is removed before the gloves enter the cleaner zone, reducing the risk that cardboard dust, fibres, or other contaminants are carried into the controlled environment.  
  • ISO 11193 Explained: The Global Standard for Single-Use Medical Examination Gloves (2026 Guide)
    ISO 11193 Explained: The Global Standard for Single-Use Medical Examination Gloves (2026 Guide)
    Aug 28, 2026
    ISO 11193 is the international standard specification for single-use medical examination gloves. It has two parts: ISO 11193-1 covers gloves made from rubber latex or rubber solution (natural rubber latex, nitrile rubber, polychloroprene, styrene-butadiene rubber, and thermoplastic elastomers), and ISO 11193-2 covers gloves made from poly(vinyl chloride), PVC. The current edition of Part 1 is ISO 11193-1:2020. When a glove carries ISO 11193 compliance, it means the lot has been tested for freedom from holes, dimensions, physical properties (force at break and elongation), and biocompatibility. 1. Scope and Structure ISO 11193-1:2020 (third edition, published August 2020) specifies requirements for packaged sterile or bulk non-sterile rubber gloves used in medical examinations and diagnostic or therapeutic procedures, and for handling contaminated medical materials. Gloves are classified by type and finish: Type 1: gloves made primarily from natural rubber latex Type 2: gloves made primarily from nitrile rubber latex, polychloroprene rubber latex, styrene-butadiene rubber solution or emulsion, or thermoplastic elastomer solution Finishes: textured, smooth, powdered, or powder-free surface Part Material Typical glove Current edition in wide use ISO 11193-1 Rubber latex / rubber solution (natural rubber, nitrile, polychloroprene, SBR, TPE) Medical examination gloves ISO 11193-1:2020 ISO 11193-2 Poly(vinyl chloride), PVC Vinyl examination gloves ISO 11193-2 2. Key Test Requirements ISO 11193-1 sets requirements across five areas, with test methods drawn from other standards: Attribute Requirement (typical) Test method Length Min 220-230 mm depending on size ISO 11193-1 dimensional requirements Thickness Min 0.05-0.08 mm at palm/finger (varies by finish) ISO 4648 Freedom from holes AQL 1.5 (water leak test, ISO 2859-1 sampling) Water leak test Force at break >= 7 N before aging; >= 6 N after aging (median) ISO 37 Elongation at break >= 500% before aging; >= 400% after aging ISO 37 Aging 7 days at 70 degrees C ISO 188 Powder residue (powder-free) Maximum powder per glove, if labeled powder-free Defined in standard Biocompatibility Cytotoxicity, sensitization, irritation ISO 10993 series Note: values above reflect typical published conformance data from major manufacturers; always verify the exact figures in the supplier batch test report. AQL stands for Acceptable Quality Limit - for medical examination gloves the hole tolerance is AQL 1.5 (maximum 1.5% of a sampled lot may leak). 3. How ISO 11193 Compares with EN 455 and ASTM D6319 Buyers often see ISO 11193, EN 455, and ASTM D6319 on the same datasheet. They test similar properties but express them differently: Property ISO 11193-1 EN 455-2 ASTM D6319 Market focus International / GCC (GSO ISO 11193-1) EU US (FDA 510(k)) Freedom from holes AQL 1.5 AQL 1.5 (EN 455-1) AQL 1.5 Force at break (exam gloves) >= 7 N (before aging), >= 6 N (after) >= 6.0 N Not used (uses MPa) Tensile strength Not specified as MPa Not specified as MPa >= 14 MPa (before and after aging) Elongation >= 500% / >= 400% Not specified >= 500% / >= 400% Aging protocol 7 days at 70 degrees C 7 days at 70 degrees C 7 days at 70 degrees C (per ASTM D7160) Biological evaluation ISO 10993 series EN 455-3 ISO 10993 series The key insight: EN 455-2 and ISO 11193 express strength as force at break in Newtons, while ASTM D6319 expresses it as tensile strength in MPa. Both are valid; they measure different quantities (absolute force vs force per unit cross-section). 4. Where ISO 11193 Is Used GCC / Middle East: GSO has adopted ISO 11193-1 as GSO ISO 11193-1:2020, making it a common acceptance standard in Saudi Arabia, the UAE, and other Gulf states Southeast Asia, Latin America, and Africa: widely referenced in public hospital procurement Global manufacturers: most export factories certify to ISO 11193-1 plus EN 455 and/or ASTM D6319 for dual-market coverage China: the national standard GB 10213 is technically identical to ISO 11193-1 5. Buyer Checklist for ISO 11193 Compliance Confirm the edition: request the exact standard and edition (e.g., ISO 11193-1:2020) named on the certificate and test report Check the AQL: verify the water-leak AQL is 1.5 for medical examination use Request full physical property data: force at break and elongation before AND after aging Verify biocompatibility: ISO 10993 test reports (cytotoxicity, sensitization, irritation) Review labeling: packaging symbols per ISO 15223, date of manufacture, batch code Confirm finish: powder-free vs powdered and the powder residue test, if applicable Cross-check with market rules: GSO ISO 11193-1 for GCC, EN 455 for EU, ASTM D6319 + FDA 510(k) for US Data sources: ISO 11193-1:2020 (ISO.org); ISO 11193-2; GSO ISO 11193-1:2020; EN 455-1/2 series; ASTM D6319-19; ISO 2859-1; ISO 37; ISO 188; ISO 10993 series. Values cross-checked against published manufacturer conformance data. Information current as of August 2026. FAQ Q: Is ISO 11193 the same as EN 455 or ASTM D6319? A: No, but they cover similar ground. ISO 11193 is the international standard for single-use examination gloves; EN 455 is the EU harmonized standard (Part 1 holes, Part 2 physical properties, Part 3 biological evaluation, Part 4 shelf life); ASTM D6319 is the US standard for nitrile examination gloves linked to FDA 510(k) clearance. Many export gloves are certified to two or three of these. Key differences: EN 455-2 and ISO 11193-1 report strength as force at break in Newtons, while ASTM D6319 reports tensile strength in MPa. Q: Does ISO 11193 apply to PVC (vinyl) gloves? A: Yes. ISO 11193-2 is the part that specifies requirements for single-use examination gloves made from poly(vinyl chloride). Part 1 covers rubber materials (natural rubber latex, nitrile rubber, polychloroprene, SBR, TPE). When a datasheet simply says ISO 11193, check which part is referenced - Part 1 for rubber, Part 2 for PVC. Q: What AQL does ISO 11193 require for pinholes? A: ISO 11193-1 requires an Acceptable Quality Limit of 1.5 for freedom from holes when tested with the water leak test and sampled per ISO 2859-1. This means no more than 1.5% of the sampled lot may leak. AQL 1.5 is the same threshold used by EN 455-1 and ASTM D6319 for medical examination gloves. Q: How should a buyer verify ISO 11193 compliance? A: Ask the supplier for the certificate and, more importantly, the batch test report showing the standard and edition, the batch code, the water-leak AQL result, force at break and elongation before and after aging, powder residue (if powder-free), and ISO 10993 biocompatibility data. The report must cover the specific batch being shipped, not a historical sample. You can also verify that the test laboratory is accredited (e.g., ISO/IEC 17025). Q: Can a glove be certified to ISO 11193 and EN 455 at the same time? A: Yes, this is common practice. Export factories typically certify a single product to ISO 11193-1 (international/GCC), EN 455 (EU), and ASTM D6319 (US) so the same glove can be sold across markets. Because the test methods for holes and aging are harmonized, dual certification usually requires little extra testing beyond the physical property differences (force at break vs tensile strength).  
  • Glove Tensile Strength and Elongation - How Physical Property Tests Define Nitrile Glove Quality
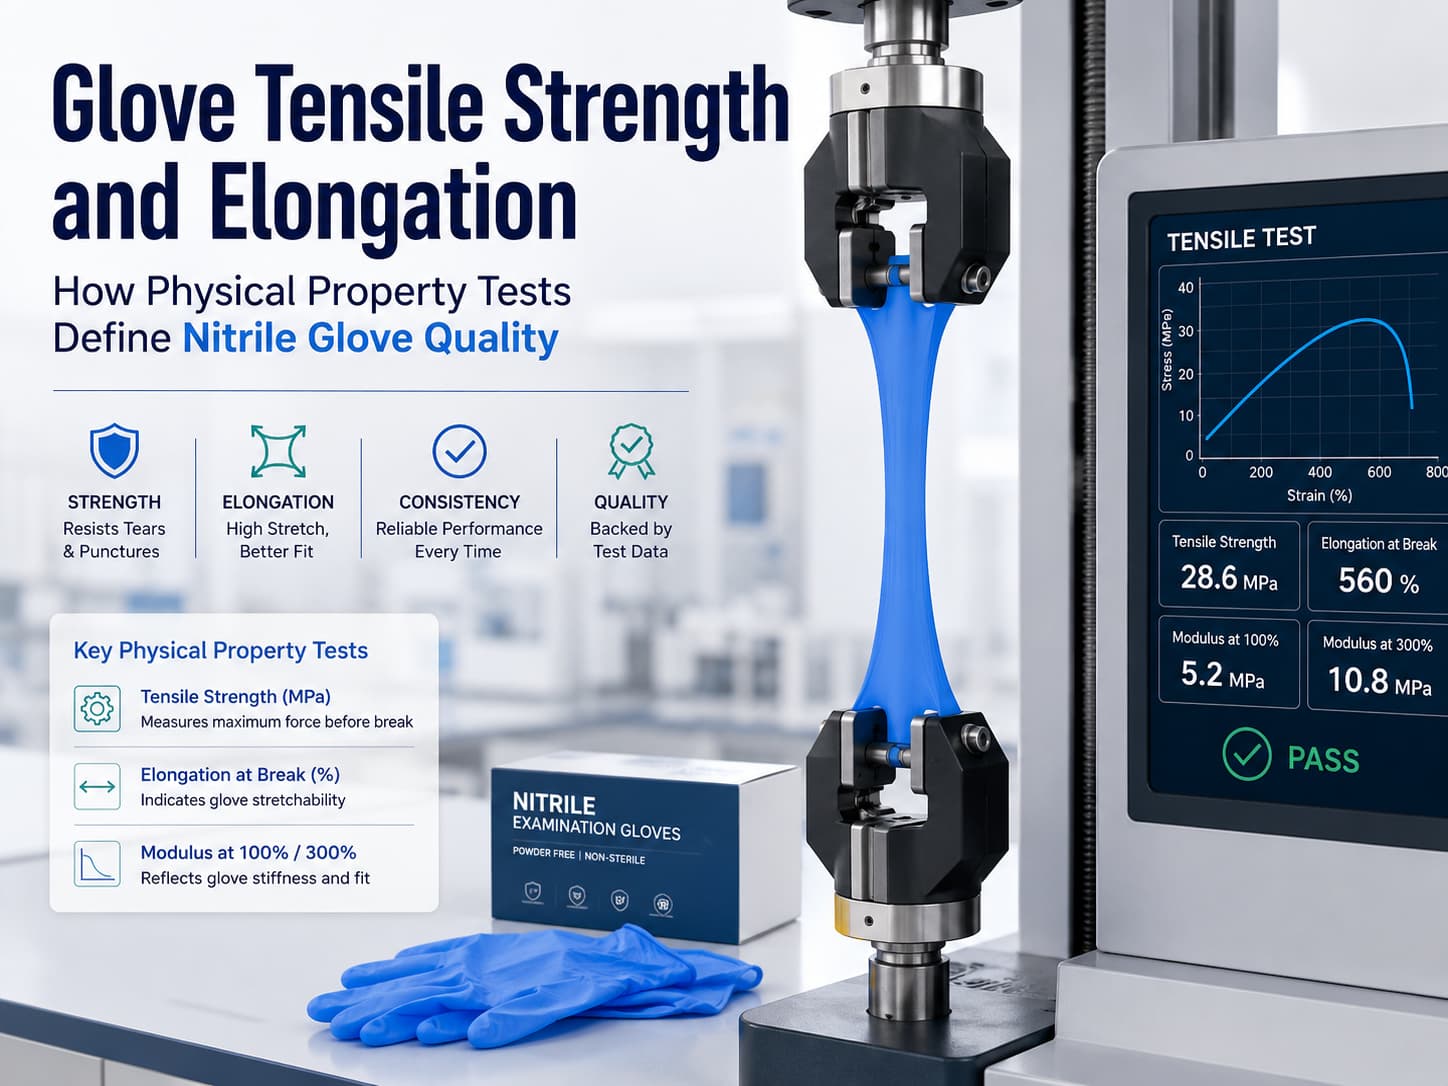
    Glove Tensile Strength and Elongation - How Physical Property Tests Define Nitrile Glove Quality
    Aug 27, 2026
    Tensile strength and elongation at break are the two numbers that tell you whether a nitrile glove will tear in use. This guide explains how the tests work, the requirements in ISO 11193, EN 455-2, and ASTM D6319, and how buyers should read a test report. Tensile strength is the maximum force a glove material can withstand before it breaks, expressed in megapascals (MPa); elongation at break is how far the material stretches before tearing, expressed as a percentage of original length. Together they determine whether a glove tears when you pull it on, when you flex your fingers, or when it snags on a sharp edge. A glove that fails either test fails its barrier function - a torn glove is no longer protection. This guide explains how these tests are performed, what the major standards require, and how to read the numbers on a datasheet. 1. Why Physical Properties Matter A disposable glove is a barrier. Tensile strength and elongation are the two properties that decide how well that barrier survives real use: Donning: the glove is stretched over the hand; low elongation means it tears during donning Movement: repeated finger flexing stresses the material; weak material develops holes or tears Snagging: contact with instruments, rings, or rough surfaces concentrates force at a point Aging: materials degrade over time; the after-aging values tell you if the glove will still perform at the end of its shelf life 2. How the Tests Work The test procedure is standardized across ISO 11193, EN 455-2, and ASTM D6319: Thirteen gloves are sampled from one lot Dumbbell-shaped (dog-bone) test pieces are cut from the palm, back of hand, or cuff, avoiding textured areas, along the longitudinal axis Test pieces are conditioned for at least 16 hours at 23 +/- 2 degrees C and 50 +/- 10% relative humidity Each piece is pulled at a crosshead speed of 500 mm/min until it breaks The median value of the 13 results is reported For the after-aging value, a second set is aged 7 days at 70 degrees C (per ISO 188) before testing The median (not the average) is used, which makes the result robust to a single outlier piece. 3. Requirements by Standard Each standard expresses the requirement differently - Newtons (force at break) or MPa (tensile strength): Standard Strength metric Requirement (median) Elongation at break Aging ISO 11193-1 Force at break >= 7 N before aging; >= 6 N after aging >= 500% before; >= 400% after 7 days at 70 degrees C (ISO 188) EN 455-2 Force at break >= 6.0 N (examination); >= 3.6 N (PVC/thermoplastic); >= 9.0 N (surgical) Not specified in EN 455-2 7 days at 70 degrees C (ISO 188) ASTM D6319 Tensile strength >= 14 MPa before and after aging >= 500% before; >= 400% after 7 days at 70 degrees C Two practical takeaways: EN 455-2 deliberately does not specify elongation - elongation figures on a datasheet come from the ASTM or ISO specification Newtons and MPa are not interchangeable: MPa normalizes force by the cross-section of the test piece, so comparing them directly across standards is not valid 4. What the Numbers Mean for Buyers Higher force at break / tensile strength generally means a more durable glove that resists punctures and tears. Higher elongation means the glove stretches further before breaking - important for donning and dexterity. But the balance matters: Too weak (low force at break): gloves tear during donning or use Too stiff (low elongation): gloves feel tight, restrict movement, and crack Too elastic (very high elongation with low strength): gloves feel baggy and snag easily Typical material behavior (indicative ranges, not requirements): Material Tensile strength (typical) Elongation at break (typical) Feel Natural rubber latex 18-24 MPa 650-750% Very elastic, high strength Nitrile rubber 14-25 MPa 400-600% Strong, good elasticity Vinyl (PVC) 8-13 MPa 250-350% Stiffer, lower strength 5. Common Mistakes When Reading a Datasheet Comparing MPa and N directly: not valid - they measure different quantities Ignoring after-aging values: the glove will degrade; after-aging is the true shelf-life performance Quoting a single batch: physical properties vary by batch; request reports for the actual lot shipped Missing the median note: standards report the median of 13 pieces; a strong outlier should not be presented as the result Assuming higher is always better: very high strength can mean a stiffer glove; match the property profile to the task 6. Buyer Checklist Request force at break (ISO 11193 / EN 455-2) or tensile strength (ASTM D6319) before AND after aging Check elongation at break before and after aging (where specified) Verify the report covers the exact batch code being shipped Confirm the test lab is accredited (ISO/IEC 17025) Match the property profile to the application: thin high-tactility gloves for precision, thicker higher-strength gloves for industrial use Keep reports on file for audits and customer requests Data sources: ISO 11193-1:2020; EN 455-2:2015; ASTM D6319-19; ISO 37; ISO 188; ISO 2859-1; ISO/IEC 17025. Requirements verified against official standard summaries and published manufacturer conformance data (including FDA 510(k) summaries). Typical material ranges are indicative and vary by formulation. Information current as of August 2026. FAQ Q: What is a good tensile strength for nitrile gloves? A: Under ASTM D6319, nitrile medical examination gloves must have a tensile strength of at least 14 MPa before and after accelerated aging. Most commercial nitrile gloves test well above this, typically in the 18-25 MPa range. For non-medical industrial gloves, requirements vary by standard and use case, but higher tensile strength generally means better puncture and tear resistance. Q: Why do gloves need to pass tests after accelerated aging? A: Gloves degrade over time due to oxidation, heat, and humidity. The accelerated aging test (7 days at 70 degrees C, per ISO 188) simulates years of shelf life in about a week. Passing after aging proves the glove will still meet its strength and elongation requirements at the end of its declared shelf life. A glove that only passes before aging may become brittle or weak before you use it. Q: What is the difference between force at break (N) and tensile strength (MPa)? A: Force at break (Newtons) is the absolute force needed to break the test piece. Tensile strength (MPa) divides that force by the cross-sectional area of the test piece, normalizing for thickness. EN 455-2 and ISO 11193 use force at break; ASTM D6319 uses tensile strength. They are not directly comparable, which is why you cannot convert one to the other without knowing the test piece geometry. Q: Which standard should my supplier test report reference? A: It should reference the standard required by your market: EN 455-2 for EU medical use, ASTM D6319 for US medical use (with FDA 510(k)), and ISO 11193-1 for international and GCC tenders. Many suppliers report multiple standards on one datasheet. Whatever the standard, the report must show before- and after-aging values, the batch code, and an accredited test laboratory. Q: Does higher tensile strength always mean a better glove? A: Not necessarily. Higher strength improves tear and puncture resistance, but it often comes with lower elongation and a stiffer feel. A very strong, stiff glove may be uncomfortable and restrict dexterity. The best glove matches its physical property profile to the task: high tactility and moderate strength for precision work, high strength and durability for industrial use. Always look at strength AND elongation together.
  • Latex Protein Allergy and Glove Selection: Type I Reactions, Protein Testing, and Nitrile Alternatives (2026 Guide)
    Latex Protein Allergy and Glove Selection: Type I Reactions, Protein Testing, and Nitrile Alternatives (2026 Guide)
    Aug 25, 2026
    Latex protein allergy is a Type I IgE-mediated reaction that can escalate from skin irritation to anaphylaxis. This guide explains how latex proteins trigger allergy, how protein testing works (ASTM D5712, ISO 12243), and why nitrile gloves are the safer, cost-effective choice for healthcare and industry in 2026. Latex protein allergy (Type I) is one of the most serious occupational health issues associated with medical gloves. Unlike contact dermatitis, which is a skin reaction, Type I latex allergy is an immediate hypersensitivity reaction mediated by immunoglobulin E (IgE). It can progress from hives to life-threatening anaphylaxis in minutes. This guide explains the science behind latex protein allergy, the testing used to quantify it, and why switching to nitrile rubber gloves has become standard practice in healthcare and industry. 1. What Is Type I Latex Protein Allergy? Latex gloves are made from natural rubber latex, a milky fluid harvested from the Hevea brasiliensis tree. This fluid naturally contains proteins, and some of these proteins are antigens: when they contact skin, mucous membranes, or the bloodstream, the immune system of sensitive individuals produces IgE antibodies. On re-exposure, the antibodies trigger the release of histamine and other chemicals, producing symptoms within minutes. Because Type I reactions are systemic and potentially fatal, they are distinct from Type IV contact dermatitis (a delayed T-cell-mediated reaction caused by chemicals such as accelerators). The table below summarizes the differences. Feature Type I (Immediate) Type IV (Delayed) Mechanism IgE-mediated T-cell mediated Trigger Latex proteins Accelerators, vulcanization chemicals Onset Minutes 6-48 hours Symptoms Hives, rhinitis, asthma, anaphylaxis Itchy rash, blisters, cracking Glove material involved Natural rubber latex Latex and nitrile (accelerator chemicals) Severity Can be life-threatening Usually local, rarely systemic Prevention Latex-free gloves (nitrile, PVC, TPE) Accelerator-free formulations 2. Who Is at Risk? Prevalence studies from the 1990s-2000s, when powdered latex gloves were widely used, reported latex protein sensitization in roughly 8-17% of healthcare workers with heavy exposure. Rates have fallen sharply in markets that moved to powder-free and low-protein gloves, but risk groups remain: Healthcare and dental workers with years of glove exposure Patients with spina bifida or repeated surgeries (frequent latex exposure via catheters and gloves) Workers in laboratories, food processing, and cleaning who wear latex gloves daily Atopic individuals (those with existing allergies, eczema, or asthma) Workers in glove manufacturing itself 3. Symptoms and Diagnosis Type I reactions present across three severity levels: Skin: contact urticaria (hives) within minutes at the contact site Respiratory: sneezing, runny nose, itchy eyes, asthma-like wheezing Systemic: angioedema, hypotension, anaphylaxis (medical emergency) Diagnosis is confirmed by an allergist using skin-prick tests with latex extract, specific IgE blood tests, or a supervised glove-use test. Anyone with suspected latex allergy should be evaluated before anaphylaxis occurs, and should carry an epinephrine auto-injector if confirmed. 4. Protein Testing Standards Because proteins are the trigger, quantifying them is the core of latex glove safety. Three methods dominate: ASTM D5712: modified Lowry method for analysis of protein in natural rubber and its products; the most commonly cited test for water-extractable protein on glove surfaces ISO 12243: determination of water-extractable protein in medical gloves made from natural rubber latex using the modified Lowry method; a harmonized approach for international markets EN 455-3: the EU biological evaluation standard, which requires protein testing (extractable latex proteins play a central role in latex allergy) plus powder and endotoxin limits Buyers should request the protein test report (usually expressed in micrograms per gram, mg/g, or micrograms per square decimeter) with every latex glove batch. Powder-free latex gloves typically have far lower protein content than powdered ones, because powder binds and carries proteins into the air, where they are inhaled. 5. Regulatory Actions Against Latex Exposure FDA ban on powdered surgeon and powdered patient examination gloves (effective January 2017) because powder increases protein exposure and aerosolization EU medical device rules (currently Regulation (EU) 2017/745) require biocompatibility evaluation of gloves, including sensitization testing under ISO 10993-10 WHO and CDC guidance has long recommended latex-free protocols where Type I allergy risk exists Many hospitals and food facilities have adopted 100% latex-free policies for this reason 6. Why Nitrile Rubber Gloves Are the Safer Choice Nitrile rubber (acrylonitrile butadiene rubber, ACN + butadiene) is a synthetic polymer that contains no latex proteins at all. It delivers the barrier performance that latex is famous for, without the allergy risk. Property Natural rubber latex Nitrile rubber Latex proteins Present - Type I allergy risk None Barrier vs pathogens Excellent (EN 455 certified) Excellent (EN 455 / ASTM D6319 certified) Chemical resistance Moderate Better (oils, solvents, many chemicals) Puncture resistance Good Better Tensile strength Very high (18+ MPa typical) High (14+ MPa per ASTM D6319) Elongation Very high (650-700%+) 400-600% Cost (2026) Moderate Competitive; premium in acute shortages Type IV risk Low-moderate Low-moderate (accelerator chemicals; accelerator-free options exist) The practical result: nitrile gloves now dominate medical examination, dental, laboratory, food service, and industrial applications in most markets. 7. Building a Latex-Free Procurement Policy Audit current usage: identify every latex glove and latex-containing product (catheters, tourniquets, bandages) in the facility Choose alternatives: nitrile rubber for exam and general tasks; PVC or TPE for low-risk food handling; specialized gloves for chemo and cleaning Verify certification: EN 455 (EU) or ASTM D6319 with FDA 510(k) (US) for medical use; keep batch test reports on file Train staff: communicate the difference between Type I and Type IV, and how to recognize symptoms Label high-risk areas: maintain clearly marked latex-free zones in ORs, dental suites, and allergy clinics Review TDS data: request protein test reports from any supplier that still supplies latex gloves Data sources: prevalence literature on latex protein sensitization (8-17% in high-exposure healthcare workers, pre-powder-free transition); FDA final rule banning powdered gloves (2016, effective 2017); ASTM D5712; ISO 12243; EN 455-3; EN ISO 21420 (formerly EN 420) for general glove requirements; ISO 10993-10. Information current as of August 2026; verify regulatory status before procurement decisions. FAQ Q: What is the difference between Type I and Type IV glove allergies? A: Type I is an immediate IgE-mediated reaction to latex proteins, with symptoms appearing within minutes (hives, rhinitis, asthma, and in severe cases anaphylaxis). Type IV is a delayed T-cell-mediated contact dermatitis caused by chemicals such as accelerators, appearing 6-48 hours after exposure, and it can affect both latex and nitrile glove wearers. Nitrile gloves eliminate Type I risk (no latex proteins) but some users may still develop Type IV reactions to accelerator chemicals, which is why accelerator-free nitrile gloves exist. Q: How do I know if I am allergic to latex? A: A doctor (allergist) can confirm latex allergy with a skin-prick test using latex extract, a specific IgE blood test, or a supervised glove-use test. Common signs include hives where the glove touched the skin, sneezing, itchy eyes, or wheezing within minutes of putting on a latex glove. Anyone with suspected Type I latex allergy should be formally evaluated, because repeated exposure can escalate from mild symptoms to anaphylaxis. Q: Can nitrile gloves cause latex allergy? A: No. Nitrile rubber (acrylonitrile butadiene rubber, ACN + butadiene) is fully synthetic and contains no latex proteins, so it cannot trigger Type I latex allergy. Nitrile gloves are the standard replacement for latex in healthcare, dental, laboratory, and food settings. Note that a small number of users may develop Type IV contact dermatitis from accelerator chemicals in nitrile gloves; accelerator-free formulations are available for these cases. Q: Do powder-free latex gloves still carry allergy risk? A: Yes, a reduced but real risk. Powder-free latex gloves have much lower protein content and produce far less airborne protein than powdered gloves, which is why sensitization rates fell after the FDA powdered-glove ban (effective January 2017). But even low-protein latex can trigger symptoms in already-sensitized individuals. For facilities with any Type I allergy concern, latex-free nitrile gloves remain the safer choice. Q: What protein tests should a buyer request from a latex glove supplier? A: Request batch-level reports for ASTM D5712 (modified Lowry, water-extractable protein) and, for EU shipments, evidence of EN 455-3 compliance which covers protein, powder, and endotoxin testing. ISO 12243 is the international method for the same modified Lowry analysis. Check that the protein value is expressed in a clear unit (e.g., micrograms per gram or per square decimeter) and that the report covers the specific batch being shipped, not a historical sample.  
  • Disposable Glove Receiving Inspection: Incoming Quality Assurance Checklist (2026)
    Disposable Glove Receiving Inspection: Incoming Quality Assurance Checklist (2026)
    Aug 21, 2026
    Receiving inspection is the structured process of verifying that a delivered glove shipment matches the purchase order, the supplier's test claims, and the applicable standards - before the goods are accepted and paid for. It is the buyer's last independent checkpoint before quality problems become expensive problems. This guide covers the documents to verify, the visual checks, the statistical sampling plan, on-site tests, and the accept-hold-reject decision framework. 1. Direct Answer: What Receiving Inspection Is and Why It Matters Receiving inspection (incoming quality assurance, or AQA) is performed at the warehouse when goods arrive. Its purpose is to protect the buyer from three risks: (1) wrong or short product (incorrect size mix, count, or model), (2) non-conforming quality (failed AQL, damaged packaging, missing certifications), and (3) unverifiable claims (a supplier that says "compliant" but provides no batch evidence). In volatile markets, batch-level documentation and spot checks are the difference between catching a problem in 48 hours and discovering it after the gloves are already distributed to users. 2. Documents to Verify Before Opening Cartons Check the documents first - they determine what the shipment claims to be. Verify that lot numbers, quantities, and descriptions match the purchase order. Document What to check Why it matters Packing list Carton count, quantity, lot numbers, model/size mix Confirms shipment matches the PO Certificate of Conformity (CoC) / Analysis (CoA) Batch-level test results: AQL water leak, tensile strength, elongation, dimensions Proves the batch passed manufacturing QC Standards certificates EN 455, ASTM D6319, EN ISO 374, ISO 13485 (as applicable) Confirms the product is certified to the required standard EU Declaration of Conformity Product ID, standards cited, manufacturer signature Required for legal EU placement Labels / carton marking Size, quantity, lot number, expiry date, manufacturer ID, barcode/UDI Enables traceability and stock rotation Regulatory registration references FDA 510(k) K-number, EUDAMED UDI-DI for medical gloves Confirms legal market access 3. Visual Inspection of Cartons and Labels Carton condition: Check for crushing, water damage, or torn outer boxes. If outer cartons are damaged, inspect inner boxes before accepting. Label accuracy: Verify size, quantity, lot number, and expiry date printed on cartons match the packing list. Expired or near-expiry stock should be flagged. Lot consistency: Multiple lot numbers in one shipment are normal - but every lot must have its own CoC/CoA and test report. Single-lot shipments are easier to trace. Pallet and wrapping: Check for moisture, pests, or foreign objects. Document any anomalies with photos. 4. Statistical Sampling per ISO 2859-1 Sample size follows ISO 2859-1 (ANSI/ASQ Z1.4), using the lot size, the inspection level (typically General Level II), and the AQL from your contract (AQL 1.5 for medical exam gloves, AQL 2.5/4.0 for industrial). Examples for AQL 1.5, General Level II: Lot size (pieces) Sample size (pieces) Accept (Ac) Reject (Re) 2,801 - 8,000 125 5 6 8,001 - 22,000 200 7 8 22,001 - 110,000 315 10 11 110,001 - 500,000 500 14 15 500,001+ 800 21 22 Sample randomly from multiple cartons and multiple layers of the pallet - not from the first box you open. Record which cartons were sampled for traceability. Never reduce the sample size below the standard; the acceptance numbers lose their statistical meaning. 5. On-Site Physical Tests Several checks can be performed at the warehouse without laboratory equipment: Water leak (AQL) test: Fill a sampled glove with about 1,000 mL of water, hold 1-2 minutes, and check for droplets or wet spots. Any leak = barrier failure. Perform on a statistically valid sample. Visual defect check: Inspect sampled gloves for holes, tears, discoloration, embedded particles, or powder anomalies. Thickness spot check: If you have a micrometer, measure palm and finger thickness and compare to the TDS/specification (in mil or mm). Elasticity check: Gently stretch a sampled glove - it should return to shape without tearing or whitening (stress whitening indicates degraded polymer). Powder check (powder-free products): Shake a glove over dark fabric; visible powder residue indicates non-conformance. Laboratory tensile and elongation testing (ASTM D412 / EN 455-2) requires a tensile testing machine - for full verification, send samples to an ISO 17025 accredited laboratory. 6. Accept - Hold - Reject Decision Framework Decision Trigger Action ACCEPT All document, visual, and sampling checks pass Document results, release to stock, file the inspection report with the CoC/CoA HOLD Minor non-conformity: label misprints, damaged outer cartons with intact inner boxes, missing copies of certificates (verifiable) Quarantine the lot, notify the supplier, set a resolution deadline (e.g., 7 days) for replacement documents or re-labeling REJECT Failed AQL, wrong product/size mix, missing or non-matching certificates, expired or near-expiry stock Quarantine the lot, issue a written rejection with photos and test evidence, negotiate return/credit per contract, keep retain samples 7. Records and Traceability Every inspection produces a record. Keep at least: inspection date, PO number, supplier, lot numbers, sample size and acceptance/rejection result, on-site test results, photos of anomalies, and the disposition (accept/hold/reject). Retain samples from each inspected lot for 6-12 months for medical products. A complete inspection file is the evidence base for claims, audits, and regulatory inquiries - and it feeds directly into supplier scorecards for the next sourcing decision. Data sources: ISO 2859-1 (sampling procedures for inspection by attributes); EN 455 series; ASTM D6319 / D412; ISO 17025 (laboratory accreditation); EU MDR 2017/745 (UDI requirements). Sampling table values are from ISO 2859-1 General Inspection Level II, AQL 1.5. Information current as of August 2026. FAQ Q: What is a receiving inspection for disposable gloves and why is it important? A: Receiving inspection (incoming quality assurance) is the process of verifying that a delivered glove shipment matches the purchase order, the supplier's test claims, and the applicable standards BEFORE the goods are accepted and paid for. It matters because in volatile markets a meaningful share of shipments shows issues - wrong size mix, damaged cartons, missing batch reports, or in rare cases failed AQL. Accepting defective goods without evidence makes claims and returns much harder. A structured receiving inspection protects the buyer's quality, safety, and budget. Q: What documents must accompany a compliant glove shipment? A: A compliant shipment should include: (1) packing list with quantities, carton counts, and lot numbers; (2) Certificate of Conformity / Certificate of Analysis with batch-level test results (AQL water leak, tensile strength, elongation, dimensions); (3) applicable standards certificates (EN 455, ASTM D6319, ISO 13485, or EN ISO 374 for chemical gloves); (4) EU Declaration of Conformity if selling in the EU; (5) labels with size, lot number, expiry date, and manufacturer ID; and (6) for medical gloves, regulatory registration references such as FDA 510(k) K-number or EUDAMED UDI-DI. Verify that lot numbers on documents match lot numbers on cartons. Q: How many gloves should be sampled for an AQL inspection? A: Sampling follows ISO 2859-1 (ANSI/ASQ Z1.4). For a medical glove shipment with AQL 1.5 at General Inspection Level II, a lot of 35,001-150,000 gloves requires a sample of 315 gloves with acceptance number 10 and rejection number 11. For a smaller lot of 8,001-22,000 gloves, the sample is 200 gloves with acceptance 7 and rejection 8. Use the lot size and AQL from your contract to look up the correct sample size - never sample fewer than the standard requires, or the inspection loses statistical meaning. Q: Can we test the water leak (AQL) on-site at our warehouse? A: Yes, a basic on-site water leak test is feasible: fill a sampled glove with about 1,000 mL of water and inspect for droplets or wet spots after 1-2 minutes. Any leak means the glove fails barrier integrity. This catches gross defects such as holes and tears, but does not substitute for laboratory tensile and elongation testing, which requires a tensile testing machine. For full verification, send samples to an accredited laboratory (ISO 17025) and request the batch test report from the manufacturer. Q: What should we do if a shipment fails inspection? A: Follow a three-tier decision: (1) ACCEPT - all checks pass; document and release to stock. (2) HOLD - minor non-conformities such as label misprints or damaged outer cartons with intact inner boxes; quarantine, notify the supplier, and decide on rework or re-labeling with a time limit. (3) REJECT - failed AQL, wrong product, missing certificates, or non-conforming labeling; quarantine the lot, formally reject in writing, and negotiate return or credit per contract terms. Always photograph non-conformities, keep retain samples, and issue a written inspection report within 48 hours.  
  • Reusable vs Disposable Gloves: A Task-Based Comparison (2026 Guide)
    Reusable vs Disposable Gloves: A Task-Based Comparison (2026 Guide)
    Aug 20, 2026
    Disposable or reusable? The answer depends on the task, the contamination risk, and the cost per use. Compare barrier integrity, standards, and true economics with this task-based glove selection guide. The core difference is simple: disposable gloves are designed for one use or one procedure, then discarded; reusable gloves are designed for multiple uses with cleaning in between. The deciding factor is never just price per box - it is barrier integrity, contamination risk, and true cost per use for the specific task. This guide gives procurement teams and safety officers a task-based framework to choose correctly. 1. Direct Answer: What Separates the Two Categories Disposable gloves (nitrile rubber, latex, vinyl, polyethylene) are manufactured to be worn once and thrown away. Their barrier is guaranteed until first use. Reusable gloves (heavy-duty nitrile, neoprene, natural rubber, PVC) are worn repeatedly for months or years and cleaned between uses. The fundamental trade-off: disposable gloves guarantee a fresh barrier but create waste; reusable gloves save material but their barrier degrades with every flex, chemical contact, and cleaning cycle - and they can carry contamination from one task to the next. 2. Material and Design Comparison Attribute Disposable gloves Reusable gloves Typical materials Nitrile rubber, latex, vinyl (PVC), polyethylene Heavy-duty nitrile, neoprene, natural rubber, PVC Intended lifespan Single use / single procedure Months to years with cleaning Barrier integrity Guaranteed until first use Degrades with use, flexing, and cleaning Cross-contamination risk None if changed correctly High unless rigorously cleaned and segregated Typical thickness 3-8 mil (0.08-0.20 mm) 10-60 mil (0.25-1.50 mm) for chemical gloves Key standards EN 455, ASTM D6319, EN ISO 374, EN 388 EN ISO 374, EN 388, EN ISO 21420 (formerly EN 420) Cleaning required None - discard Wash, dry, inspect after every use Cost per use Higher at high frequency Lower at high frequency, if maintained 3. Task-Based Selection Matrix Use the table below as a first-pass decision tool. When in doubt, choose the option that protects against the worst-case contamination or injury scenario. Task category Contamination / injury risk Recommended choice Healthcare - patient contact, exams Blood, body fluids, pathogens Disposable medical gloves (EN 455 / ASTM D6319, AQL 1.5) Healthcare - chemotherapy handling Hazardous drug permeation Disposable chemo-tested nitrile (ASTM D6978 where applicable) Food handling - ready-to-eat Foodborne pathogens, cross-contamination Disposable food-grade gloves Cleanroom / electronics Particles, electrostatic discharge Disposable cleanroom gloves (ISO 14644 classification) Heavy chemical handling (industry) Concentrated acids, solvents, oils Reusable chemical-resistant gloves (EN ISO 374) Abrasion / puncture-heavy work Mechanical injury Reusable heavy-duty gloves (EN 388) Household cleaning, gardening Mild chemicals, dirt Reusable household gloves Short, changing tasks (assembly, inspection) Varies by step Disposable nitrile rubber 4. Where Disposable Gloves Are Mandatory In three settings, single-use disposable gloves are not a preference - they are a regulatory and safety requirement: Healthcare: Medical examination and surgical gloves must be single-use per EN 455 (EU) and ASTM D6319/D3578 (US). Reusing gloves between patients is a recognized cause of cross-contamination and healthcare-associated infections. Food service: Direct handling of ready-to-eat food requires single-use gloves per US FDA Food Code and EU food contact practice (Regulation 1935/2004). Reusable gloves cannot be reliably cleaned to food-safety standards between uses. Cleanrooms and pharma: Particle control requires fresh, certified gloves per cleanroom protocols (ISO 14644). A reused glove sheds particles and carries contamination. 5. Where Reusable Gloves Are the Right Call Reusable gloves are the correct choice when the glove is the tool for a repeated task, the contamination is limited to the glove material itself, and the exposure justifies the higher initial investment: Chemical handling: EN ISO 374-rated reusable gloves are tested for permeation against specific chemicals over hours - disposable gloves are tested for shorter exposure and are not suitable for immersion or prolonged contact with concentrated chemicals. Mechanical work: EN 388-rated reusable gloves resist abrasion, cuts, and puncture - disposable exam gloves offer no such protection. High-frequency, low-contamination tasks: Household cleaning, dishwashing, and light industrial tasks where the same glove can be reused safely with proper cleaning. 6. True Cost Comparison Comparing only box prices is misleading. The correct metric is cost per protected task. The example below shows a stylized comparison for an industrial facility. Scenario Purchase price Uses per glove Cost per task (approx.) Disposable nitrile rubber, 100-box (100 pcs) $8-15 per box 1 $0.08-0.15 per task Disposable nitrile rubber, case of 10 boxes $70-130 per case 1 $0.07-0.13 per task Reusable chemical glove, pair $12-25 per pair 100-200 uses (18-24 months) $0.06-0.25 per task (incl. cleaning) Reusable household glove, pair $3-8 per pair 50-150 uses (6-12 months) $0.02-0.16 per task (incl. cleaning) Reusable gloves win on cost only when they are actually reused many times, cleaned correctly, and never used for contamination-prone tasks. If a reusable glove is discarded early because of damage or contamination, its cost per use quickly exceeds that of disposables. 7. Five Decision Questions Does the task involve blood, body fluids, or food? If yes -> disposable, always. Is the glove exposed to concentrated chemicals for extended periods? If yes -> reusable chemical-resistant gloves (EN ISO 374). Does the task change between uses? If the next use could bring different contamination -> disposable. Will the glove be used many times per day, every day? If yes and contamination is low -> reusable can be economic. Can cleaning and inspection be guaranteed between uses? If not -> disposable. Data sources: EN 455 series (EU medical gloves); ASTM D6319 / D3578 (US medical gloves); EN ISO 374 (chemical protection); EN 388 (mechanical risk); EN ISO 21420 (formerly EN 420, general requirements); US FDA Food Code; EU Regulation 1935/2004. Cost figures are illustrative ranges for comparison, current as of August 2026 - obtain current quotes for budgeting. FAQ Q: What is the main difference between reusable and disposable gloves? A: Disposable gloves are designed for a single use or single procedure, then discarded. Reusable gloves are designed for multiple uses over months or years, with cleaning between uses. The critical difference is barrier integrity management: a disposable glove is guaranteed intact until first use, while a reusable glove's barrier degrades with each flex, chemical exposure, and cleaning cycle. In healthcare, food handling, and cleanroom work, single-use disposable gloves are mandatory because cross-contamination between users or tasks cannot be safely eliminated. Q: Can disposable gloves be washed and reused to save money? A: No. Washing and reusing disposable nitrile or vinyl gloves is explicitly prohibited by infection control guidelines (CDC, WHO) because washing degrades the polymer barrier, creates micro-tears, and cannot remove all contaminants. Studies show that washing gloves increases the risk of cross-contamination rather than reducing it. The cost savings are illusory when a single healthcare-associated infection costs far more than a box of gloves. If a task requires repeated protection, choose correct single-use discipline, or a properly maintained reusable glove for non-medical tasks. Q: When does a reusable glove make economic sense? A: Reusable gloves make economic sense for repeated, high-frequency tasks where the glove is not exposed to contamination that requires disposal - for example, household cleaning, gardening, dishwashing, light assembly, or handling consistent chemicals. The cost per use of a good reusable nitrile or PVC glove (kept 0.5-2 years with proper cleaning) can be 5-20x lower than using disposable gloves for the same number of tasks. However, if the glove contacts blood or food, or becomes contaminated, or if the task changes between uses, disposable is the correct choice. Q: What standards apply to reusable vs disposable gloves? A: Disposable medical gloves follow the EN 455 series (EU) or ASTM D6319/D3578 (US), with AQL 1.5 water-leak testing. Disposable industrial gloves may follow EN ISO 374 for chemical protection and EN 388 for mechanical risk. Reusable chemical gloves follow EN ISO 374 (permeation testing), EN 388 (mechanical), and EN ISO 21420 (formerly EN 420) for general requirements. The key point: a glove's standard tells you the intended use - always match the certified standard to the actual task, not the brand or color. Q: Are reusable gloves ever acceptable in food service? A: In food service, single-use disposable gloves are the standard for direct food contact (US FDA Food Code, EU Regulation 1935/2004 and HACCP practices). Reusable gloves are generally not acceptable for direct handling of ready-to-eat food because they cannot be reliably cleaned between uses and create cross-contamination risk. Reusable gloves can be used for non-food tasks such as washing dishes and cleaning equipment, but they must be color-segregated and never used for direct food contact.
  • Tattoo and Beauty Industry Gloves - A Procurement Guide for Inking, Piercing, and Cosmetology
    Tattoo and Beauty Industry Gloves - A Procurement Guide for Inking, Piercing, and Cosmetology
    Aug 18, 2026
    Tattoo, piercing, and beauty studios are high-exposure environments. Artists work with blood, needles, inks, pigments, acetone, acrylate monomers, and a long list of chemicals - while touching clients directly. Choosing the right disposable gloves is not a style choice; it is an infection control and occupational safety decision. This guide explains the risks by service type, compares glove materials for beauty applications, and gives a practical procurement checklist for studios. 1. Why Tattoo and Beauty Work Requires Dedicated Gloves Unlike general office environments, tattoo and beauty services create three distinct exposure routes: Bloodborne pathogens: Tattoo, piercing, and permanent makeup involve needles that break the skin. Hepatitis B, Hepatitis C, and HIV are transmitted through blood contact. Single-use gloves are the primary barrier between the artist's hands and the client's blood. Chemical exposure: Nail services use acetone, acrylate monomers, and UV gels. Hair coloring involves para-phenylenediamine (PPD), ammonia, and bleach. These chemicals can cause contact dermatitis (Type IV allergy) and are absorbed through the skin. Ink and pigment exposure: Tattoo pigments contain heavy metals and organic colorants. Pigment staining of the hands is not just cosmetic - it indicates skin contact with materials that should stay under the skin or on the surface. Gloves in these settings must provide a certified barrier, chemical resistance where needed, and enough tactile sensitivity for precision work. Nitrile rubber (acrylonitrile butadiene rubber, ACN + butadiene) meets all three requirements, which is why it dominates the professional studio market. 2. Risk Profile by Service Type The glove requirement differs by service. The table below maps the main hazards and the recommended glove for each service. Service Main Hazards Recommended Glove Tattoo Bloodborne pathogens, ink pigments, needle sticks, disinfectants Nitrile rubber, 4-6 mil (0.10-0.15 mm), black or blue Body piercing Bloodborne pathogens, metal contact, needle sticks Nitrile rubber, 4-6 mil (0.10-0.15 mm) Permanent makeup / microblading Blood + pigment, fine needle control Nitrile rubber, 4 mil (0.10 mm), maximum tactility Nail services (acrylic, gel) Acetone, acrylate monomers, UV gel Nitrile rubber, 4-6 mil (0.10-0.15 mm) Hair coloring PPD, ammonia, bleach, oxidation dyes Nitrile rubber, 3-4 mil (0.08-0.10 mm) Facials and skincare Low infection risk, product actives Nitrile rubber or vinyl, 3 mil (0.08 mm) Salon cleaning Disinfectants, bleach, detergents Nitrile rubber, 4-6 mil (0.10-0.15 mm) 3. Glove Materials Compared for Beauty Applications Three materials appear in studio glove boxes: nitrile rubber, latex, and vinyl (PVC). Their differences determine when each is acceptable. Property Nitrile rubber Latex Vinyl (PVC) Barrier vs bloodborne pathogens Excellent (EN 455 / ASTM D6319 certified models) Excellent (EN 455 certified models) Lower - higher permeability, weaker tensile strength Resistance to acetone / monomers Good Poor - degrades with solvents Poor Resistance to PPD / hair dyes Good Moderate Poor Latex protein allergy risk None Type I allergy risk (8-17% sensitization reported in exposed workers) None Tactile sensitivity High (4 mil models) Very high Low to moderate Durability during long sessions Good Good Poor - tears easily Phthalate concerns (EU REACH) None None Yes - phthalate plasticizers under scrutiny Typical use in studios Professional standard for all services Legacy - being phased out Low-risk short tasks only 4. Black Nitrile Gloves - Why Color Matters in Studios Black nitrile gloves are the same nitrile rubber as blue or white versions, with carbon black pigment added. Color does not change barrier performance, AQL, or tensile strength. But in professional studios, black offers practical advantages: Ink and pigment hiding: Black hides tattoo ink, dye, and pigment stains that make blue or white gloves look contaminated during a session. Visual contrast: Black gloves against skin tones make ink lines and needle position easier for the artist to see during fine work. Professional image: Black gloves are associated with premium studios and are the expected choice in many tattoo markets. Caution for food-adjacent work: In food service, black gloves can be confused with other dark materials and some food codes discourage them. In beauty-only settings this is not an issue. When ordering black nitrile gloves, verify they carry the same certification as other colors from the same manufacturer (EN 455, ASTM D6319, AQL 1.5 where applicable). 5. Fit, Texture, and Comfort for Long Sessions Tattoo sessions can last hours. Glove comfort directly affects artist performance. Key specification points: Thickness: 4-6 mil (0.10-0.15 mm) balances sensitivity and durability; 3 mil (0.08 mm) for maximum fingertip feel on fine line work. Texture: Textured fingertips improve grip on tattoo machines and tools; beaded cuffs prevent roll-down and glove-to-skin contact at the wrist. Sizing: Correct fit matters more than brand. Measure hand circumference at the palm; sizes follow the EN ISO 21420 (formerly EN 420) sizing codes where applicable. Dexterity: On the standard dexterity scale of 1 to 5, studio gloves should deliver level 4-5 for fine motor tasks. Powder-free: Always choose powder-free gloves. Powder can contaminate open wounds, interfere with pigment adhesion, and trigger irritation. 6. Regulatory Considerations for Studio Gloves Studio gloves should meet at least one recognized standard. In the EU, medical-grade disposable gloves follow EN 455 (examination gloves) or EN ISO 374 (chemical protection). In the US, nitrile examination gloves follow ASTM D6319 with FDA 510(k) clearance. For beauty chemicals, EN ISO 374 chemical permeation testing adds confidence against acetone and monomers. Gloves are not cosmetics, but they contact skin and clients, so choose certified products and keep the batch test reports (AQL water leak, tensile, elongation) on file. Waste disposal of used gloves should follow local medical or biohazard waste rules where blood contact is possible. 7. Procurement Checklist for Tattoo and Beauty Studios Standardize on nitrile rubber for all services involving blood, chemicals, or precision work. Stock black nitrile for artist-facing tasks and blue/white nitrile for general studio use, with color-segregated storage. Buy a size mix - most studios order S, M, and L in a ratio matched to staff hand sizes; add XS and XL for flexibility. Request batch-level test reports (AQL 1.5 water leak, tensile strength, elongation) with every order. Verify certifications (EN 455, ASTM D6319, or EN ISO 374 as applicable) and keep certificates on file. Order in volume with buffer stock - studios use 20-60 pairs per artist per day depending on service volume. Train staff on glove change discipline: between clients, after touching surfaces, and after any contamination. Data sources: WHO Guidelines on Infection Prevention and Control; CDC Guidelines for Environmental Infection Control; occupational health literature on latex protein sensitization (reported 8-17% in exposed healthcare and beauty workers); EU REACH regulation on phthalates; EN 455 / ASTM D6319 / EN ISO 374 standards. Information current as of August 2026; verify regulatory status before procurement decisions. FAQ Q: Why are nitrile gloves the standard choice in tattoo studios instead of latex? A: Latex gloves were once standard in tattoo studios but carry two problems: Type I latex protein allergy (occupational health studies report latex protein sensitization in roughly 8-17% of healthcare and beauty workers regularly exposed to powdered latex gloves) and weaker resistance to ink solvents and disinfectants. Nitrile rubber gloves provide a comparable or better barrier against bloodborne pathogens, resist inks, acetone, and common disinfectants better, and eliminate the latex protein allergy risk. Most professional tattoo artists switched to nitrile rubber in the 2010s, and black nitrile became the visual standard. Q: Do black nitrile gloves provide the same protection as blue or white ones? A: Yes. Black nitrile gloves are made from the same nitrile rubber (acrylonitrile butadiene rubber, ACN + butadiene) with carbon black pigment added. The pigment does not change barrier properties, tensile strength, or the AQL water-leak rating. Black is preferred in tattoo and beauty work because it hides ink and pigment stains, provides visual contrast against skin tones, and gives a professional studio look. Always verify that black gloves carry the same certification (EN 455, ASTM D6319, AQL 1.5) as other colors from the same manufacturer. Q: What thickness of nitrile gloves should a tattoo artist use? A: Most tattoo artists work with 4-6 mil (0.10-0.15 mm) nitrile gloves for a balance of tactile sensitivity and durability. Thinner gloves (3 mil) give maximum fingertip feel for line work but tear more easily during long sessions; thicker gloves (6-8 mil) last longer but reduce sensitivity. In the beauty industry, 3-4 mil is common for short tasks (hair coloring, facials), while 4-6 mil is recommended for nail services involving acetone and acrylate monomers. Thickness is always expressed in mil or mm. Q: Are vinyl gloves acceptable for beauty work? A: Vinyl (PVC) gloves can be used for low-risk, short-duration beauty tasks such as shampooing, makeup application, or light cleaning where no blood, chemicals, or sharps are involved. Vinyl has weaker tensile strength and higher permeability than nitrile rubber, so it is NOT recommended for tattoo, piercing, permanent makeup, nail monomer handling, or any task with blood contact or strong chemicals. Vinyl also contains phthalate plasticizers, which face increasing EU REACH scrutiny. For professional studios, nitrile rubber is the safer default. Q: How often should gloves be changed during a tattoo or beauty session? A: Change gloves between every client, and change mid-procedure whenever gloves are contaminated, torn, or after touching non-sterile surfaces such as phones, door handles, or equipment. In tattoo work, artists typically change gloves after setting up the station, before handling the tattoo machine, and after any interruption. For a single client, use a fresh pair for setup and a fresh pair for the procedure if the setup pair touched surfaces - never reuse a pair. Single use means single use.
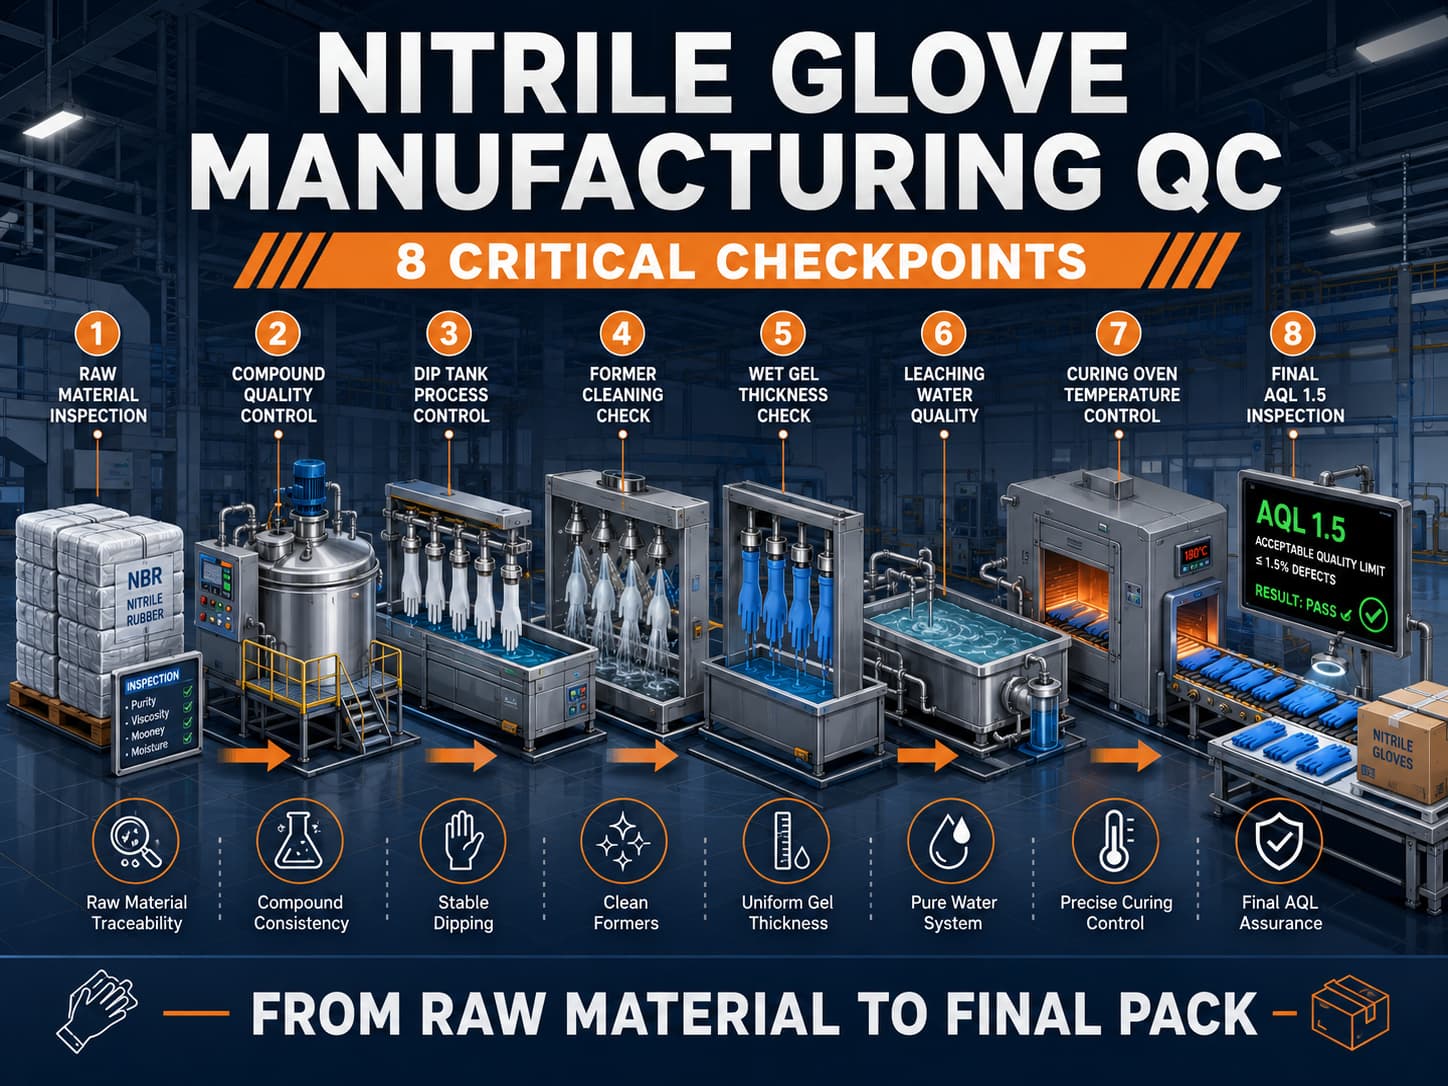
  • Nitrile Glove Manufacturing Quality Control - 8 Critical Checkpoints from Raw Material to Final Pack
    Nitrile Glove Manufacturing Quality Control - 8 Critical Checkpoints from Raw Material to Final Pack
    Aug 14, 2026
    Nitrile rubber glove manufacturing is a continuous chemical process with multiple stages, each requiring specific quality controls. A single missed checkpoint can lead to AQL failure, pinhole defects, or shelf life issues that compromise end-user safety. This guide walks through the 8 critical QC checkpoints from incoming raw material to final packaging, with specific control limits, test frequencies, and corrective actions. Essential reading for quality engineers, procurement auditors, and sourcing professionals evaluating disposable glove suppliers. 1. The 8 Checkpoints at a Glance # Checkpoint Control Parameter Test Frequency 1 Raw nitrile rubber incoming Mooney viscosity, ACN content, volatile matter Per incoming lot 2 Compound preparation Crosslinker/accelerator/stabilizer dispersion, pH Every batch (800-1,200 kg) 3 Dipping tank conditions Temperature, coagulant concentration, viscosity Continuous / every 30 min 4 Former cleanliness Surface contamination, residual polymer, temperature Per cycle (every 60-90 sec) 5 Wet gel film thickness Coagulant dip time, residence time, draft speed Every hour 6 Leaching tank water quality pH, temperature, water hardness, surfactant level Continuous monitoring 7 Curing oven profile Temperature uniformity, dwell time, hot spots Per oven load 8 Final AQL and shelf life Water leak (AQL 1.5), tensile, elongation, powder Per batch (ISO 2859-1) 2. Checkpoint 1: Raw Nitrile Rubber Incoming Inspection Raw nitrile rubber (NBR) is the core material. Incoming inspection verifies that each shipment meets specifications before release to production. Key parameters: Mooney viscosity: Typically 70-100 ML(1+4) at 100 degrees C. High viscosity indicates harder-to-process material. Low viscosity may indicate degradation or off-spec production. Control: reject lots outside the specification window. Acrylonitrile (ACN) content: Typically 28-33% for glove-grade NBR. Higher ACN gives better oil resistance but lower flexibility. Control: verify by Kjeldahl nitrogen analysis or FTIR. Volatile matter: Should be below 0.5% by weight. High volatile content can cause porosity and pinholes during dipping. Control: oven-dry a sample for 2 hours at 105 degrees C. Contamination check: Visual inspection of bales for foreign particles, dirt, or discoloration. Control: reject contaminated bales. 3. Checkpoint 2: Compound Preparation The raw nitrile rubber is compounded with crosslinkers (typically zinc oxide and sulfur or peroxide), accelerators (carbamates, thiurams, mercaptobenzothiazoles), stabilizers, pigments (for colored gloves), and processing aids. Critical QC parameters during compounding include: Mixing time and temperature: Insufficient mixing causes uneven dispersion; excessive mixing causes scorch (premature crosslinking). Control: mill or internal mixer temperature below 100 degrees C; mixing time per recipe. Dispersion quality: Visual inspection of compound sheets for streaks, lumps, or undispersed material. Control: pass through a straining mesh before transfer to dipping tank. pH control: The dipping compound should be maintained within a defined pH range (typically 9-11) for stable viscosity and proper coagulation. Control: continuous pH monitoring with auto-dosing. Viscosity: The compound viscosity affects film thickness and consistency. Control: Brookfield viscosity measurement at 25 degrees C, recorded every batch. 4. Checkpoint 3: Dipping Tank Conditions The dipping tank holds the compounded nitrile rubber latex. Key parameters: Parameter Typical Range Control Method Frequency Compound temperature 22-28 degrees C Heat exchanger with PID control Continuous Compound viscosity 20-60 cP Brookfield viscometer, automatic Every 30 min Total solids content 35-45% Refractometer or gravimetric oven drying Every hour pH 9-11 Continuous pH probe with auto-dosing Continuous Mechanical agitation Continuous, controlled speed Variable-speed impeller Continuous Coagulant dip concentration Calcium nitrate 5-15% + calcium carbonate Auto-dosing pump Continuous 5. Checkpoint 4: Former Cleanliness and Surface The former (ceramic or metal mold) defines the glove shape. Contamination causes pinholes and defects. Critical controls: Surface cleanliness: Formers are washed with acid/caustic solutions and brushed between cycles. Control: visual inspection for residual polymer; sample swab testing weekly for residual contaminants. Surface temperature: Affects film formation. Control: 50-70 degrees C depending on formulation; PID-controlled heater. Coagulant coating uniformity: The coagulant dip (often calcium nitrate in alcohol) must form a uniform thin film on the former surface before latex dipping. Control: visual inspection and dip weight measurement. 6. Checkpoint 5: Wet Gel Film Thickness Wet gel thickness determines the final glove thickness. Controls: Dipping time: Longer dip = thicker film. Control: programmable dip timer, deviation less than +/- 0.5 second. Withdrawal speed: Affects film uniformity. Control: programmable hoist, deviation less than +/- 5% of set speed. Drying tunnel temperature and humidity: Affects film formation. Control: 80-120 degrees C with controlled humidity. Wet film thickness measurement: Sampled using a wet film gauge or by calculation from glove weight and surface area. Control: every hour, track trend. 7. Checkpoint 6: Leaching Tank Water Quality After dipping, the wet gel is washed in a leaching tank to remove excess surfactants, calcium salts, and unbound additives. Critical parameters: Parameter Target Why It Matters Frequency Water pH 6.5-8.0 Affects surfactant removal Continuous Water temperature 40-60 degrees C Drives leaching kinetics Continuous Water conductivity < 50 microS/cm (ion exchange) Prevents re-deposition of ions on glove surface Continuous Surfactant level 0.1-0.5% non-ionic Maintains wetting for next dipping stage Daily Residence time 10-30 min Sufficient time for leaching Per cycle Water turnover Continuous bleed + makeup Prevents buildup of impurities Continuous 8. Checkpoint 7: Curing Oven Profile The curing (vulcanization) oven crosslinks the nitrile rubber to give final mechanical properties. Critical controls: Temperature uniformity: Multi-zone oven with independent PID control per zone. Monitor with a multipoint thermocouple probe weekly to verify no hot or cold spots. Dwell time: Typically 15-30 minutes at 120-140 degrees C. Control: conveyor speed and oven length. Airflow: Proper airflow prevents cool spots and removes volatiles. Control: weekly airflow verification at multiple positions. 9. Checkpoint 8: Final AQL and Shelf Life Verification Final QC ensures only conforming gloves leave the factory. Tests per batch: Test Method Acceptance Criterion Sampling Water leak (AQL 1.5) Fill glove with 1,000 mL water, inspect for leaks after 2 min No droplets ISO 2859-1, General Level I, AQL 1.5 Tensile strength ASTM D412 (dumbbell from cuff) >= 14 MPa (ASTM D6319) 3 samples per batch Elongation at break ASTM D412 >= 500% (ASTM D6319) 3 samples per batch Powder residue ASTM D6319 section 9 (if powder-free) <= 2 mg per glove 2 samples per batch Dimensions (width, length, thickness) ASTM D6319 section 6 Within specified tolerance 5 samples per batch Accelerated aging ASTM D7160 (70 degrees C, 7 days) Pass tensile + AQL after aging 1 sample set per week Visual defects Inspection booth No holes, tears, discoloration, foreign matter 100% or AQL sampling If any test fails, the batch is reworked or rejected. Batch-level test reports are generated and must accompany each shipment for procurement verification. 10. Buyer Audit Checklist When auditing a potential supplier, verify the 8 checkpoints are actively controlled. Request: Recent (within 6 months) raw material test records Compound batch records with mixing time, temperature, viscosity Dipping tank monitoring logs (24-hour continuous) Former cleaning CIP (clean-in-place) records and swab test results Wet film thickness trend charts Leaching tank water analysis records (pH, conductivity, surfactant) Oven temperature profiling reports from each oven Final AQL test reports per batch with K-values per ISO 2859-1 Accelerated aging reports (ASTM D7160 or EN 455-4) Customer complaint and CAPA (Corrective Action/Preventive Action) log FAQ Q: What are the most critical QC checkpoints in nitrile glove manufacturing? A: The 8 most critical QC checkpoints are: (1) raw nitrile rubber incoming inspection (Mooney viscosity, ACN content), (2) compound preparation (crosslinker, accelerator, stabilizer dispersion), (3) dipping tank temperature and coagulant concentration, (4) former (mold) cleanliness and surface temperature, (5) wet gel film thickness control, (6) leaching tank pH and water quality, (7) curing oven temperature uniformity and dwell time, and (8) final post-cure inspection (AQL water leak, tensile strength, elongation, powder residue). Each checkpoint has specific control limits and frequency. Q: How often should QC testing be performed during production? A: Frequency varies by checkpoint. Raw material testing is per-lot (each incoming shipment). Compound preparation testing is every batch (typically 800-1,200 kg). Dipping and former checks are continuous or every 30 minutes. Wet gel thickness is typically checked every hour. Leaching tank pH is monitored continuously. Curing oven profiling is done per oven load. Final AQL is per batch per ISO 2859-1 sampling plans. The key is that QC data is traced to specific lot/batch numbers for traceability. Q: What is the difference between AQL 1.5 and AQL 2.5 for nitrile gloves? A: AQL (Acceptable Quality Level) is the maximum acceptable percentage of defective items in a sample. AQL 1.5 means the sample can have at most 1.5% defective units; AQL 2.5 allows up to 2.5%. AQL 1.5 is required for medical examination gloves (EN 455-1, ASTM D6319). AQL 2.5 is typical for industrial gloves. A lower AQL means tighter quality but more rejected units during production. Most manufacturers achieve actual defect rates well below the AQL limit. Q: What causes pinholes in nitrile rubber gloves and how are they detected? A: Pinholes are tiny defects that compromise the glove's barrier function. Common causes include: contaminated former surface (residual polymer, dirt), improper coagulant dipping (uneven film formation), foreign particles in the compound, air bubbles trapped in latex, and mechanical damage during stripping. Pinholes are detected by the water leak test (AQL 1.5 sampling): the glove is filled with water and visually inspected for droplets or wet spots. Failed gloves are rejected. Q: How is shelf life determined for nitrile medical examination gloves? A: Shelf life is determined through accelerated aging tests per ASTM D7160 or EN 455-4 protocols. Samples are aged at elevated temperature (typically 70 degrees C) for a defined period, then tested for tensile strength, elongation, and AQL water leak. The aging time is extrapolated to estimate real-time shelf life at 25 degrees C storage. Typical nitrile rubber gloves have a 3-5 year shelf life when stored properly (10-30 degrees C, below 65% relative humidity, away from direct sunlight).  
  • ASTM D6319 Explained: US Standard for Nitrile Examination Gloves (2026 Guide)
    ASTM D6319 Explained: US Standard for Nitrile Examination Gloves (2026 Guide)
    Aug 12, 2026
    ASTM D6319 is the US standard specification for nitrile examination gloves intended for medical application. This certification interpretation guide explains the scope of ASTM D6319, its key test requirements, the FDA 510(k) clearance linkage, and how it compares to the European EN 455 series. Essential reading for procurement professionals sourcing gloves for the US healthcare market or dual-certifying products for both the US and EU. 1. What Is ASTM D6319? ASTM D6319, titled "Standard Specification for Nitrile Examination Gloves for Medical Application," is maintained by ASTM International (formerly American Society for Testing and Materials). First published in 1999, it is regularly revised to reflect current manufacturing practice and biocompatibility science. The standard establishes requirements for nitrile rubber gloves used in medical examinations, diagnostic procedures, and patient contact in healthcare settings. ASTM D6319 is recognized by the US FDA and is referenced as a consensus standard for 510(k) premarket notification submissions for medical examination gloves. Gloves that demonstrate compliance with ASTM D6319, along with biocompatibility testing per ISO 10993, are eligible for 510(k) clearance. 2. Scope and Application ASTM D6319 applies to nitrile rubber examination gloves used in medical examinations, diagnostic procedures, and patient contact. The standard covers five key attribute groups: Attribute Group What It Covers Test Reference Physical dimensions Length, width, palm thickness, finger thickness ASTM D6319 section 6 Physical properties Tensile strength, elongation at break before and after accelerated aging ASTM D6319 section 7 Freedom from holes Water leak test (AQL 1.5) ASTM D6319 section 8, ISO 2859-1 Powder residue Maximum powder amount (if labeled powder-free) ASTM D6319 section 9 Biocompatibility Cytotoxicity, sensitization, irritation (referenced to ISO 10993) ISO 10993 series 3. Key Test Requirements Physical Properties (Before and After Accelerated Aging) ASTM D6319 specifies tensile strength and elongation at break both before and after accelerated aging. The aging protocol is per ASTM D7160 or equivalent. Minimum values depend on the thickness category, but typical requirements are: Property Before Aging After Aging (7 days @ 70 degrees C) Test Reference Tensile strength >= 14 MPa >= 14 MPa ASTM D412 Elongation at break >= 500% >= 400% ASTM D412 Tensile strength (finger) >= 18 MPa >= 18 MPa ASTM D412 Freedom from Holes (Water Leak Test) The water leak test is the critical barrier integrity check. Gloves are filled with a defined volume of water and visually inspected for leaks. The Acceptable Quality Level (AQL) is 1.5, meaning the sample can have at most 1.5% defective units when sampled per ISO 2859-1 (equivalent to ANSI/ASQ Z1.4). Sampling plans typically reference General Inspection Level I or II with single sampling. The water leak test is harmonized with EN 455-1, meaning gloves that pass one test generally pass both. Dual-certified gloves typically use the same leak test method. Powder Residue Limit ASTM D6319 limits the powder residue on powder-free gloves to 2 mg per glove maximum. The test method fills the glove with water and rinses, then evaporates the rinsate and weighs the residue. Powdered gloves have no residue limit under ASTM D6319, but FDA regulations and purchaser requirements increasingly favor powder-free products. 4. Biocompatibility Requirements (ISO 10993) ASTM D6319 does not specify biocompatibility test methods itself but requires that the glove pass cytotoxicity, sensitization, and irritation tests per the ISO 10993 series. Typically, the following tests are required: Test Purpose Method Reference Cytotoxicity (MEM elution) Detect cell-killing substances ISO 10993-5 Sensitization (LLNA or GPMT) Detect allergic contact dermatitis potential ISO 10993-10 Irritation (intracutaneous reactivity) Detect skin irritation potential ISO 10993-10 Acute systemic toxicity (optional) Detect systemic toxic effects ISO 10993-11 Testing must be performed on the finished glove, not just the raw nitrile rubber. A change in formulation (different accelerator, plasticizer, pigment) typically requires re-testing per ISO 10993. 5. ASTM D6319 vs EN 455 Comparison ASTM D6319 and EN 455 (series 1-4) both certify nitrile examination gloves for medical use. For dual-certified products, the differences are minor but worth understanding. Requirement ASTM D6319 EN 455 Series Region of recognition US (FDA 510(k)) EU (MDR 2017/745) Freedom from holes AQL 1.5 1.5 (EN 455-1) Tensile strength (before aging) >= 14 MPa >= 7 MPa (EN 455-2) Elongation (before aging) >= 500% >= 500% (EN 455-2) Powder residue limit <= 2 mg/glove (powder-free) <= 2 mg/glove (EN 455-3 powder-free) Protein content limit Not applicable (nitrile) <= 50 microg/g for latex; not applicable to nitrile Biocompatibility ISO 10993 required ISO 10993 required (EN 455-3) Shelf life determination ASTM D7160 EN 455-4 The most notable difference is tensile strength: ASTM D6319 requires a minimum of 14 MPa before aging (and same after aging), while EN 455-2 requires only 7 MPa before aging. ASTM D6319 is more stringent on tensile strength, which is one reason many manufacturers dual-certify to ASTM D6319 first and then add EN 455. 6. FDA 510(k) Clearance Process To market nitrile examination gloves in the US, manufacturers must obtain FDA 510(k) clearance. The 510(k) pathway requires: Predicate device identification: Demonstrate substantial equivalence to a legally marketed predicate device. Performance testing: Compliance with ASTM D6319 (plus biocompatibility per ISO 10993). Labeling review: Compliance with 21 CFR 801 (medical device labeling). Quality system: Manufacturing under FDA Quality System Regulation (21 CFR 820, transitioning to QSR harmonized with ISO 13485). User fee: Standard FDA user fee (currently approximately $24,000 for a 510(k) submission, with small-business discounts available). After clearance, the glove is listed in the FDA 510(k) database with the K-number. Importers and distributors should verify the K-number on each shipment's documentation. 7. Procurement Checklist for ASTM D6319 Gloves Verify FDA 510(k) clearance - Check the FDA 510(k) database for an active K-number for the glove model. Request the ASTM D6319 test report - Confirm compliance with physical properties, water leak, and powder residue limits. Request the ISO 10993 biocompatibility report - Confirm cytotoxicity, sensitization, and irritation test results on the finished glove. Verify shelf life data - Request ASTM D7160 or EN 455-4 accelerated aging test results. Typical nitrile rubber glove shelf life is 3-5 years under proper storage. Confirm AQL 1.5 sampling - Request batch-level AQL test reports with each shipment. Verify labeling compliance - Check 21 CFR 801 labeling: size, intended use, manufacturer, expiration date, lot number, storage conditions. Confirm US agent representation - Foreign manufacturers must designate a US Agent for FDA correspondence. Audit the manufacturer - For high-volume procurement, conduct an on-site or remote audit covering ISO 13485 quality system and ASTM D6319 production controls. FAQ Q: What is ASTM D6319 and what products does it cover? A: ASTM D6319 is the US standard specification for nitrile examination gloves for medical application. It establishes requirements for nitrile rubber gloves used in medical examinations, diagnostic procedures, and patient contact. The standard covers physical properties, dimensions, freedom from holes (water leak test), powder residue, and protein content. ASTM D6319 is referenced by the US FDA for 510(k) premarket notification clearance of medical examination gloves. Q: How does ASTM D6319 differ from EN 455 for nitrile examination gloves? A: ASTM D6319 and EN 455 series (EN 455-1, 455-2, 455-3, 455-4) both certify nitrile examination gloves for medical use, but they are regional standards. ASTM D6319 is recognized in the US (with FDA 510(k) clearance) while EN 455 is required in the EU under the Medical Device Regulation (MDR 2017/745). Many manufacturers dual-certify to access both markets. Key test differences include slightly different AQL sampling plans and protein-content limits (EN 455 limits latex protein; ASTM D6319 focuses on nitrile-specific biocompatibility per ISO 10993). Q: What AQL does ASTM D6319 require? A: ASTM D6319 sets the maximum Acceptable Quality Level (AQL) for freedom from holes (water leak test) at 1.5, in line with EN 455-1 and the general medical examination glove standard. The standard requires sampling per ISO 2859-1 (equivalent to ANSI/ASQ Z1.4). Some manufacturers voluntarily meet AQL 0.65 for surgical-grade applications. Batch-level AQL test reports are the standard requirement for procurement verification. Q: Does ASTM D6319 require biocompatibility testing? A: Yes. ASTM D6319 defers biocompatibility testing to ISO 10993 (Biological evaluation of medical devices). For nitrile examination gloves, the typical panel includes cytotoxicity, sensitization, and irritation tests. Test reports must reference the specific material formulation. A change in formulation (different accelerator, plasticizer, or pigment) may require re-testing under ISO 10993. Q: What packaging and labeling requirements does ASTM D6319 specify? A: ASTM D6319 requires that each glove be properly labeled with size, intended use (medical examination), and the manufacturer's identification. The packaging must include the expiration date (determined per ASTM D7160 or equivalent accelerated aging protocol), storage conditions, and any applicable warnings. For US sale, the label must also comply with FDA 21 CFR 801 (medical device labeling). Cartons must include the lot number for traceability.
  • PFAS-Free Disposable Gloves - What the 2027-2028 EU PFAS Restriction Means for Glove Procurement
    PFAS-Free Disposable Gloves - What the 2027-2028 EU PFAS Restriction Means for Glove Procurement
    Aug 11, 2026
    Per- and polyfluoroalkyl substances (PFAS), widely known as "forever chemicals," are facing broad regulatory restrictions across the European Union under the REACH regulation. For disposable glove buyers and procurement professionals, the 2027-2028 PFAS restriction timeline creates both compliance urgency and supply chain transition challenges. This guide explains what PFAS are, how they enter glove manufacturing, what the EU restriction requires, and how to verify PFAS-free claims when sourcing nitrile rubber gloves and other disposable gloves. What Are PFAS and Why the EU Restriction Matters PFAS are a family of over 12,000 synthetic chemicals characterized by carbon-fluorine bonds, which are among the strongest in organic chemistry. This molecular stability makes PFAS extremely persistent in the environment, bioaccumulative in human tissue, and linked to adverse health effects including certain cancers, immune suppression, and endocrine disruption. In disposable glove manufacturing, PFAS may be used in three primary ways: (1) mold-release agents that help gloves separate from ceramic formers during dipping, (2) surface treatments for oil and water repellency, and (3) fluoropolymer additives in polymer blends. While not all gloves contain PFAS, their presence in manufacturing chains is widespread enough that the EU has moved toward a comprehensive restriction. Current PFAS Use in Disposable Gloves Not all disposable gloves contain PFAS. The risk varies by material type and manufacturing process. The table below summarizes PFAS risk levels by glove type. Glove Type PFAS Risk Level Common Source of PFAS Nitrile rubber Low to Moderate Mold-release agents, surface treatments Latex (natural rubber) Low Some mold-release agents PVC (vinyl) Moderate Mold-release agents, plasticizer contamination Polyethylene Very Low Minimal processing aids needed Fluoropolymer-blend High PFAS is part of the polymer formulation EU REACH PFAS Restriction Timeline (2025-2028) The EU PFAS restriction is being advanced through the REACH Annex XV process, led by authorities from Germany, the Netherlands, Norway, Sweden, and Denmark. The restriction proposal was submitted in January 2023, and the European Chemicals Agency (ECHA) Committee for Risk Assessment (RAC) has been reviewing scope and derogations. Key milestones for glove buyers include: Phase Timeline What It Means for Glove Buyers Proposal submission January 2023 Initial restriction proposal submitted to ECHA RAC opinion formation 2024-2025 Committee opinions on scope, exemptions, transition periods Adoption decision 2025-2026 EU Commission decision on final restriction text Entry into force 2027-2028 Restriction becomes legally binding for all EU market access Transition period 2027-2030 (varies) Application-specific derogations may extend deadlines How to Verify PFAS-Free Claims Procurement teams should not rely on marketing claims alone. A credible PFAS-free declaration from a glove manufacturer should include the following elements: Laboratory test report from an ISO 17025-accredited lab using LC-MS/MS or GC-MS methods for targeted PFAS analysis List of targeted PFAS compounds including PFOA, PFOS, PFHxS, GenX, and other relevant substances, with detection limits Manufacturing process declaration confirming no PFAS-containing mold-release agents, surface treatments, or additives are used Supply chain documentation verifying that raw material suppliers also provide PFAS-free declarations Batch-level traceability allowing specific glove lots to be traced back to PFAS-free production runs Cost and Supply Chain Implications The transition to PFAS-free manufacturing will have measurable cost and supply implications. Buyers should prepare for: Short-term price increase of 3-8% as manufacturers invest in alternative mold-release agents, reformulate polymer blends, and conduct additional testing Supply tightening as non-compliant manufacturers exit the EU market, reducing available capacity Testing costs of approximately $200-500 per product line per test cycle, which may be passed through to buyers Documentation burden requiring updated TDS, safety data sheets, and compliance declarations for each SKU However, these costs should be weighed against the risk of non-compliance: product seizures at EU customs, market access loss, contract penalties, and reputational damage in ESG-conscious procurement markets. Transition Strategy for Glove Buyers Procurement teams should adopt a phased transition strategy starting immediately: Audit current portfolio - Identify which gloves in your current supply may contain PFAS and assess replacement urgency based on EU sales volume Request PFAS-free declarations from all existing suppliers with supporting lab test data Source alternative suppliers where current suppliers cannot provide PFAS-free verification Update specifications to include PFAS-free requirements in all new procurement documents and contracts Plan inventory transition to avoid stranded stock of non-compliant gloves after the restriction deadline FAQ Q: What are PFAS and why are they used in disposable gloves?A: PFAS (per- and polyfluoroalkyl substances) are a group of synthetic chemicals used in some glove manufacturing for oil and water repellency, mold-release agents during production, and surface treatments. They provide stain resistance and improve manufacturing efficiency but persist in the environment indefinitely, earning the name 'forever chemicals.' Q: When will the EU PFAS restriction take effect for gloves?A: The EU is advancing a broad PFAS restriction under REACH Annex XV, expected to enter force in 2027-2028. For disposable gloves, the transition period may vary by application, but manufacturers and buyers should prepare for compliance verification by mid-2027. The restriction covers intentionally added PFAS as well as PFAS present as impurities above threshold limits. Q: How can I verify that gloves are PFAS-free?A: Request a PFAS-free declaration from the manufacturer with supporting test data from an accredited laboratory. Common analytical methods include LC-MS/MS for targeted PFAS analysis. The declaration should reference specific PFAS compounds tested (e.g., PFOA, PFOS, GenX) and confirm levels are below detection limits or regulatory thresholds. Q: Are nitrile rubber gloves naturally PFAS-free?A: Nitrile rubber (acrylonitrile butadiene rubber) as a raw material does not inherently contain PFAS. However, PFAS may be introduced during manufacturing through mold-release agents, surface treatments, or contaminated additives. Buyers should still request explicit PFAS-free declarations even for nitrile rubber gloves to ensure the entire production chain is PFAS-free. Q: Will PFAS-free gloves cost more than traditional gloves?A: In the short term, PFAS-free gloves may carry a 3-8% cost premium due to reformulation, alternative mold-release agents, and additional testing requirements. As more manufacturers transition and scale economies improve, this premium is expected to narrow. Buyers should factor in the cost of non-compliance, which can include product recalls, market access loss, and reputational damage.
  • H2 2026 Disposable Glove Raw Material Cost Alert - Hormuz Tensions, Brent Crude, and Feedstock Pass-Through
    H2 2026 Disposable Glove Raw Material Cost Alert - Hormuz Tensions, Brent Crude, and Feedstock Pass-Through
    Aug 07, 2026
    Disposable glove manufacturing costs are driven primarily by four petrochemical feedstocks: butadiene (for nitrile rubber), acrylonitrile (for nitrile rubber), ethylene-derived PVC resin (for vinyl gloves), and natural rubber latex (for latex gloves). All four are influenced by crude oil prices and shipping route stability. In August 2026, Strait of Hormuz tensions, OPEC+ production decisions, and supply-side plant maintenance have created a complex cost picture. This alert summarizes verified market prices as of early August 2026 and explains the pass-through implications for glove buyers. 1. Brent Crude Oil: The Macro Driver Brent crude oil is the benchmark that sets the cost of naphtha, the primary feedstock for steam cracking that produces butadiene and ethylene (the building block of PVC). When Brent rises, the entire petrochemical value chain faces cost pressure. As of August 2-3, 2026, Brent crude was trading in a volatile range. On August 2, Brent closed at approximately $91.04/barrel, with WTI at $84.67. The Brent-WTI spread widened due to Middle East supply risk, as Hormuz disruptions affect Brent-priced barrels more directly. On August 3, prices dropped sharply (Brent down as much as 7.3% intraday to approximately $81.55/barrel) after news that US-Iran negotiations would resume. However, Iran stated that the Hormuz situation "will not return to pre-conflict conditions," suggesting ongoing risk premium. OPEC+ announced on August 2 that seven major producers would increase output by 188,000 barrels/day in September, the sixth consecutive monthly increase. However, analysts noted that with Hormuz shipping still constrained, the supply increase has limited short-term market impact. Indicator Value (as of Aug 2-3, 2026) Trend Source Brent crude (spot) ~$81.55-91.04/barrel Volatile; dropped Aug 3 on Iran talks news PriceOfOil.com, Sina Finance WTI crude (spot) ~$78.78-84.67/barrel Declined; US inventory surplus OilPriceNews.org Brent-WTI spread ~$6-8/barrel Widened (Hormuz risk premium) PriceOfOil.com OPEC+ September output +188,000 bpd increase Sixth consecutive monthly increase Xinhua / Sina Finance 2. Butadiene: Primary Nitrile Rubber Feedstock Butadiene is copolymerized with acrylonitrile to produce nitrile rubber (NBR), the core material for nitrile gloves. Butadiene is produced as a byproduct of ethylene steam cracking, so its supply and price are tied to both crude oil (naphtha feedstock) and cracker operating rates. As of late July 2026, butadiene CFR China was approximately $1,330/ton, up $30/ton from the prior assessment. Northeast Asia CFR was approximately $1,300/ton. Domestic East China prices ranged from 10,450 to 10,650 RMB/ton (Jiangyin and Jiangsu regions, July 24-27). South Korea FOB was $1,280/ton. The market showed firm supplier pricing sentiment, though downstream demand was lukewarm. Key factors: some plants (Northern Huajin) were in maintenance, supporting prices. However, with Fujian United and Zhejiang Petrochemical restarts, supply was expected to loosen. Downstream synthetic rubber demand was weak, capping upside. For nitrile glove buyers, butadiene at these levels means continued cost pressure but not a crisis-level spike. Butadiene Price Value (late July 2026) Change Source CFR China ~$1,330/ton Up $30/ton ECHEMI Northeast Asia CFR ~$1,300/ton Up $25/ton ECHEMI South Korea FOB ~$1,280/ton Up $30/ton ECHEMI East China domestic (Jiangyin) ~10,450 RMB/ton Stable ECHEMI Jiangsu domestic ~10,625 RMB/ton Up 25 RMB/ton ECHEMI 3. Acrylonitrile: Rising on Supply Tightness Acrylonitrile is the other monomer in nitrile rubber. Unlike butadiene, acrylonitrile prices in late July 2026 rose sharply due to supply-side factors rather than feedstock costs alone. East China port prices reached approximately 10,600-10,750 RMB/ton by July 27, 2026, up roughly 8.7% year-on-year. The rally was driven by Zhenhai Refining and Chemical reducing operating rates (from ~72% to a planned 50-60% in August) due to maintenance of a related methionine unit. Liaoning Jinfa also planned a 20-25 day shutdown of one 130,000-ton line in mid-August. The domestic capacity utilization rate was expected to drop to 68-69% in the first half of August, tightening overall supply. Industry inventories were at low levels, providing a foundation for the price increase. Sinopec East China planned to reduce contract supply for August, prompting active procurement. However, mid-to-late August restarts (Siérbang, Jilin Petrochemical, Tianchen Qixiang) were expected to add supply and partially restrain further increases. For nitrile glove manufacturers, acrylonitrile at these elevated levels adds direct cost pressure. Unlike butadiene, which is weakly supported by demand, acrylonitrile supply tightness means the cost increase is more likely to stick through Q3 2026. Acrylonitrile Price Value (late July 2026) Trend Source East China port ~10,600-10,750 RMB/ton Up ~8.7% YoY CCFGroup, ChemPriceHub Shandong spot ~10,650 RMB/ton Rising CCFGroup Industry utilization rate ~71.8% (dropping to 68-69%) Declining on maintenance ChemPriceHub Key driver Zhenhai rate cut + Jinfa shutdown Supply-side tightness ChemPriceHub 4. PVC Resin SG-5: Declining on Weak Demand PVC resin is the primary material for vinyl (PVC) gloves. Unlike nitrile rubber feedstocks, PVC resin prices have been declining in 2026, providing cost relief for PVC glove manufacturers. As of July 30-31, 2026, PVC SG-5 spot prices were approximately 4,200 RMB/ton in Shandong, 4,100 RMB/ton in Shanxi, and 4,350 RMB/ton in Inner Mongolia. This is down significantly from May-June 2026 highs above 5,000 RMB/ton. The July average was approximately 4,405 RMB/ton. The decline is driven by weak downstream demand from the construction and real estate sectors. Social inventory in East China has been drawn down, and export orders increased slightly in late July, but overall demand fundamentals remain weak. For PVC glove buyers, this means vinyl glove costs should be stable to declining in Q3 2026, though oversupply risks persist. PVC Resin SG-5 Price Value (July 30-31, 2026) Trend Source Shandong spot ~4,200 RMB/ton Declining 100ppi.com (SunSirs) Shanxi spot ~4,100 RMB/ton Declining 100ppi.com (SunSirs) Inner Mongolia spot ~4,350 RMB/ton Declining 100ppi.com (SunSirs) Xinjiang Yihua (ex-factory) ~4,350-4,600 RMB/ton Stable ChemicalBook July average ~4,405 RMB/ton Down from May/June highs ChemicalBook price index 5. Natural Rubber Latex: Stable but Supported Natural rubber latex is the primary material for latex gloves. TSR20 futures on the Shanghai Futures Exchange (SHFE) showed benchmark prices of approximately 12,830 RMB/ton for the August 2026 contract (nr2608) as of August 3, 2026. SICOM (Singapore Exchange) TSR20 futures for August 2026 were approximately 227.8 US cents/kg (~$2,278/ton). Natural rubber prices are supported by supply concerns (adverse weather in Thailand, falling production in Malaysia down 16.7% year-on-year in May 2026) and rising crude oil prices that increase synthetic rubber costs, shifting demand toward natural rubber. However, weak demand from China and the tire industry has capped upside. For latex glove buyers, costs are stable but carry upside risk if weather-driven supply disruptions intensify in Q4 2026. Natural Rubber Price Value (Aug 3, 2026) Trend Source SHFE nr2608 (Aug contract) ~12,830 RMB/ton Stable SHFE (Shanghai Futures Exchange) SHFE nr2609 (Sep contract) ~12,685 RMB/ton Slightly lower SHFE SICOM TSR20 (Aug) ~227.8 US cents/kg Stable SGX / Biggo Finance Malaysia production (May 2026) 20,198 tons Down 16.7% YoY DOSM Malaysia 6. Pass-Through Implications for Glove Buyers Material Feedstock Trend Glove Cost Impact Buyer Action Nitrile rubber Butadiene firm / ACN rising Moderate cost pressure through Q3 2026 Negotiate price-adjustment clause; monitor ICIS butadiene PVC (vinyl) Resin declining Cost relief; stable to declining Lock in favorable pricing; do not over-order Natural latex Stable with upside risk Low immediate pressure; watch Q4 weather Maintain buffer stock; monitor Thailand weather All categories Brent volatile (Hormuz risk) Shipping and feedstock cost uncertainty Include force majeure and shipping risk clauses 7. Buyer Action Checklist Monitor Brent crude and butadiene CFR China weekly as leading cost indicators for nitrile gloves Track acrylonitrile East China port prices, as supply tightness may persist through mid-August 2026 For PVC gloves, current low resin prices present a window to negotiate favorable terms Maintain 4-8 week buffer stock to avoid spot purchases during price spikes Negotiate contracts with raw material escalation clauses (threshold +/- 10%, cap 15%) Diversify suppliers across regions to mitigate Hormuz shipping route risk Require suppliers to cite specific price reference sources (ICIS, Platts, SunSirs) in cost justifications Data collection date: Prices verified via WebSearch on August 3, 2026. Sources: PriceOfOil.com, OilPriceNews.org, Sina Finance, ECHEMI, CCFGroup, ChemPriceHub, SunSirs (100ppi.com), ChemicalBook, SHFE, SGX. Please verify with the latest market quotes before making procurement decisions. FAQ Q: How does the Strait of Hormuz situation affect disposable glove costs? A: The Strait of Hormuz is a critical shipping route for Middle East crude oil and petrochemical feedstocks. Tensions in 2026 have kept Brent crude elevated (around $81-91/barrel in early August), which raises the cost of naphtha cracking and downstream monomer production (butadiene, acrylonitrile, ethylene for PVC). Higher feedstock costs eventually pass through to nitrile rubber and PVC glove manufacturing costs. Q: What is the current price of butadiene and how does it affect nitrile gloves? A: As of late July 2026, butadiene CFR China was approximately $1,330/ton (up $30/ton), with domestic East China prices around 10,450-10,650 RMB/ton. Butadiene is a primary feedstock for nitrile rubber (acrylonitrile butadiene rubber). Price increases directly raise nitrile glove production costs, though the impact is partially offset by downstream demand weakness. Q: Why is acrylonitrile prices rising in 2026? A: Acrylonitrile prices rose sharply in late July 2026 (East China port approximately 10,600-10,750 RMB/ton, up roughly 8.7% year-on-year) due to supply tightness. Zhenhai Refining and Chemical reduced operating rates for maintenance, and Liaoning Jinfa planned a shutdown. This supply squeeze, combined with low industry inventory levels, drove the price rally despite weak downstream demand. Q: Is PVC resin getting cheaper or more expensive in 2026? A: PVC resin SG-5 prices have been declining. As of July 30-31, 2026, spot prices in Shandong were around 4,200 RMB/ton and Inner Mongolia around 4,350 RMB/ton, down from May-June highs above 5,000 RMB/ton. Weak downstream demand (construction, real estate) is the primary driver. This benefits PVC glove manufacturers, but oversupply risks persist. Q: How can glove buyers protect against raw material price volatility? A: Buyers should negotiate price adjustment clauses tied to published feedstock indices (ICIS, Platts, SunSirs), maintain 4-8 week buffer stock to avoid spot purchases during price spikes, diversify suppliers across regions, and monitor Brent crude and butadiene trends as leading indicators. Contracts should define clear escalation thresholds and caps.  
1 2 3 4 5 6
A total of6pages
Contact Us
Unit 1301-1, No. 3, Xixishan Wei Road, Software Park phase III, Torch High-tech Zone,Xiamen City, Fujian Province, China
+86-592-6511055
+86 -15750719843
Subscribe

Copyright 2026@ Fujian Jixiang E-commerce Co., Ltd All Rights Reserved. Sitemap | Blog | Xml | Privacy Policy Network Supported

leave a message

Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Submit

Home

Products

whatsApp

contact